Can an NC Straightener Feeder Run Through a Coil Change?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 16,2026
Summary
Every coil change is a stop, and joining the coils removes most of it while introducing a weld that has to travel through a 3-in-1 decoiler straightener feeder and a progressive die unnoticed. This article compares four architectures, from stop-and-rethread to a twin mandrel, on what each gives the run and where each costs you. It covers what a weld does inside the die and the five numbers that decide the question on your own line.
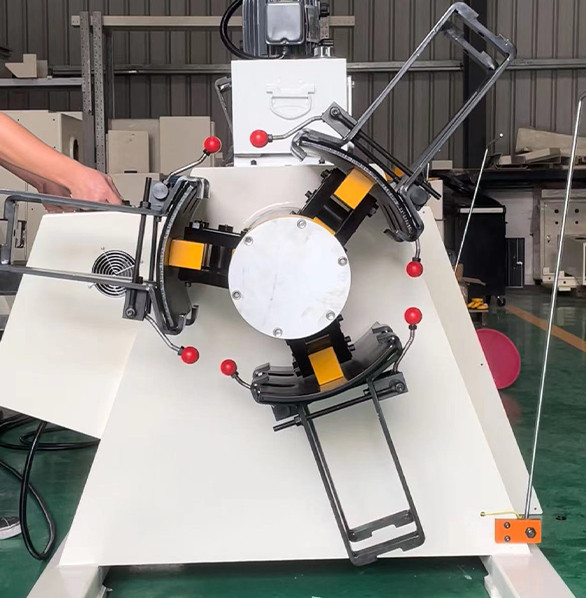
Every coil change is a stop, and every stop is paid for twice: once in lost strokes, and once in the scrap at each end of the strip.
Joining the coils removes most of that stop, and it introduces a weld that has to travel through a 3-in-1 decoiler straightener feeder and a progressive die without being noticed by either.
Whether that trade is worth making depends on how many coil changes you run per shift, and on how the die reacts to a thickness bump. Both are measurable before you spend anything.
Four Ways to Bridge a Coil Change
There are four practical architectures for keeping a line running across a coil change, and they sit on a scale from a procedural change to a capital project.
Stop and rethread. The baseline. The line stops, the strip end is cut square, the new coil is threaded and the feed is re-datumed. On a 1,300 mm line this runs 4 to 12 minutes depending on how the coil is loaded.
Manual stitch weld. The operator squares both ends and runs a short weld across the strip with a portable welder. The line stops for 3 to 6 minutes instead of 8 to 12.
Automatic shear-weld joining. A dedicated joining machine shears, aligns and welds in one cycle, typically 60 to 120 seconds, with no operator judgement on alignment.
Twin mandrel or accumulator. Either two coil positions with an automatic switch, or a loop that stores enough strip to cover the change entirely. The line does not stop at all.
The last two are the only options that remove the stop rather than shorten it. Everything else is a time reduction, and a time reduction has a much smaller payback ceiling.
A time reduction also has a floor. No procedural change can take a change below the time needed to square both strip ends and confirm the weld.
That floor is why the choice usually comes down to a joining machine or a second coil position, and rarely to a better procedure.
Matching the Method to Coil Changes per Shift
The decision turns on coil changes per shift, not on line speed. A fast line with few changes gains little from joining.
| Method | What It Gives the Run | Where It Costs You |
|---|---|---|
| Stop and rethread | No capital cost and no weld anywhere in the strip | 4 to 12 minutes of lost output per change, plus strip-end scrap on every coil |
| Manual stitch weld | Roughly half the stop time, with portable equipment only | Weld quality depends on the operator, and a poor weld reaches the die |
| Automatic shear-weld | Consistent weld every cycle and a 60 to 120 second stop | Capital cost, floor length and a maintenance routine of its own |
| Twin mandrel or accumulator | No stop at all, so the press never leaves its rhythm | The largest capital step, plus floor length the building may not have |
At two coil changes a shift, shortening the stop by five minutes returns about ten minutes a shift. That is real, and it rarely justifies an automatic joining machine on its own.
At six changes a shift the same arithmetic returns half an hour, and the picture changes completely.
The break-even is usually somewhere between three and five changes per shift, but it moves with coil weight, part pitch and how much strip is scrapped at each end.
Coil weight moves the arithmetic twice. Heavier coils mean fewer changes, but each change costs more minutes and more scrap.
Part pitch pushes it the other way. A short pitch consumes a coil quickly, so a line making small parts faces more changes per shift than one making large parts at the same tonnage.
What a Weld Does Inside the Die
A weld is a local change in thickness, hardness and, on coated strip, surface chemistry. The die sees all three.
Thickness bump. A stitch or butt weld typically stands 0.2 to 0.5 mm proud. On a progressive die with 0.08 mm clearance that is not a small feature.
Hardness change. The heat-affected zone on HSLA or stainless is harder than the parent strip, and it wears the die edge in a narrow band.
Coating damage. Welding through galvanised or pre-painted strip burns the coating off locally, which is a corrosion site on the finished part.
Alignment error. A weld that is 0.5 mm out of square tracks through the line and can lift a strip edge inside the die.
Those four effects are why most plants running a weld through a tight progressive die either slow the line for the weld pass or scrap a short zone either side of it.
The zone to scrap is not a guess. On a 1.2 mm strip it is usually 150 to 300 mm either side of the weld centreline, and it should be written into the setup sheet rather than left to the operator.
Where the weld passes is a setup decision as much as a die decision. Running it through at reduced speed costs a few seconds; running it through blind costs a die repair.
The questions that come up once a plant has costed the downtime.
Does a joining machine pay back at 3 coil changes a shift?
Typically three to five. Below three, the capital rarely pays back inside four years on downtime alone. Above five, the arithmetic usually closes quickly.
Can a 0.3 mm weld bump pass through a progressive die?
Not through a die with 0.08 mm clearance. Either slow the line and open the clearance for the weld pass, or scrap a 150 to 300 mm zone either side of it.
How much floor length does a 90-second change need?
Plan on 4 to 8 metres for a loop sized to cover a 90 second change, depending on strip width and line speed. That length is often the deciding constraint.
Does coil joining work on stainless and galvanised strip?
It works mechanically, but the weld zone needs attention. Stainless welds harder than the parent strip, and galvanised welds lose their coating locally.
What cycle time should an automatic joining machine achieve?
60 to 120 seconds from shear to weld on a 1,300 mm line is typical. Anything slower than 180 seconds loses most of the advantage over a manual stitch weld.
Five Numbers That Decide It on Your Line
Five numbers settle the question, and all five are available from the shop floor rather than from a supplier.
- Coil changes per shift. Count them for two weeks, including the short coils. The average is what the decision rests on
- Minutes per change. Time from last good part to first good part, not from stop to start. The difference is usually larger than expected
- Strip scrapped per change. Coil ends are rarely usable. Measure the scrap length and multiply by the coil count
- Coil length against part pitch. A 1,200 kg coil of 1.2 mm strip at 1,250 mm width holds roughly 100 metres. That sets how often a change arrives
- Die sensitivity to a thickness bump. If the die cannot tolerate 0.2 mm, the joining decision is really a die design decision
Where the loop or accumulator is the preferred route, its size is set by the same numbers. It has to store enough strip to cover one full change at the current line speed, with margin.
Sizing that buffer on the wrong line speed is a common error. Size it on the fastest speed the line will run, not the average, or the loop will empty mid-change.
The general relationship between line layout, loop control and the error budget is set out in the 3-in-1 decoiler straightener feeder line-setup material in our guide library.
Trial Before You Commit
A joining decision made on a quotation alone usually ends in a machine that is correct on paper and wrong on the line.
Weld one coil end and run it. Weld a real coil end with the intended process and run the joined strip through the actual die at production speed.
Inspect the parts either side of the weld. Measure the parts in the 300 mm zone either side. That is where the reject will appear if it appears at all.
Time the change honestly. Record a full manual change with a stopwatch before you decide the automatic route is worth paying for.
Check the floor and the building. An accumulator needs length and a twin mandrel needs width. Both are hard constraints once the building exists.
Ask what happens when the welder stops. Any automatic joining machine needs a manual fallback, and that fallback should be written into the operating procedure.
The trial costs a coil and half a shift. It is the cheapest part of the project and the part most often skipped.
| Trial | What It Proves | Where It Costs You |
|---|---|---|
| Weld a real coil end and run it | Whether the joint survives the straightener and the die | One coil, one shift, and a die inspection afterwards |
| Measure parts either side of the weld | How wide the scrap zone has to be | A measuring routine the operator repeats at every single change |
| Stopwatch a full manual change | The honest baseline any payback is measured against | Two hours of production time and a supervisor standing at the line |
| Check available floor length | Whether a loop or a twin mandrel fits at all | A tape measure now, or a layout redesign after the order |
Record the trial in the same format as a production run, with the parts either side of the weld measured and the reject reason written down.
If the weld zone rejects on every trial, the answer may be to route the joint to a scrap station in the die rather than to abandon joining altogether.
A welded joint on a 200 SPM line is a genuine engineering solution, not a shortcut. It stops being genuine when the weld zone is left to chance instead of being defined in the setup sheet.
Where to go next
This article belongs to the line setup and feed accuracy cluster, one layer below the specification overview. If the weld decision is settled and the feed still drifts across a coil, start with the error budget.
The Coil Line Guide Library