How Does Coil Inner Diameter Change Mandrel Choice?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Nov 4,2026
Summary
Bore size decides expansion range, and expansion range decides the drawbar, the frame length and the price. This article works the arithmetic on a 508 mm bore and a mixed 508 and 610 mm supply, then calculates the clamping force each bore needs for the same back tension. It also covers where the four common mandrel designs stop being the right answer.
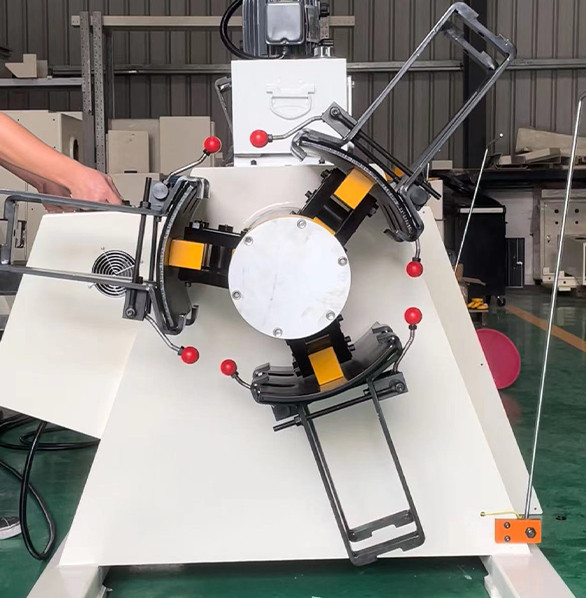
A 508 mm bore and a 610 mm bore differ by 102 mm on the drawing and by an entire mandrel design in practice. Buyers who specify one expansion range for both usually discover the gap on the first coil change.
Decoiler mandrel selection starts from the bore you will actually receive, not the bore printed on the mill certificate. That number varies by lot, by winding tension and by how the coil was stored.
Which Inner Diameters Will You Actually See?
A decoiler and a plain uncoiler are sized by the same bore arithmetic. What differs is the drive and the brake, not the segment geometry.
Three bore sizes cover most of the world's coil supply: 508 mm, 610 mm and 760 mm.
Which one arrives at your door depends on the mill, the market and the product, and it is rarely a single answer for a mixed order book.
508 mm is the common bore for narrower strip and for coils wound on lighter reels. 610 mm dominates wide, heavy coil from integrated mills.
760 mm appears on very large coils and on some aluminium and stainless supply.
The nominal figure is only the centre of a band. A 508 mm bore is routinely supplied between 500 and 514 mm, and a tightly wound coil can measure 8 mm under nominal at the inner wraps.
A mandrel sized to 508 exactly will not enter it.
| Bore | Where it comes from | What it forces on the mandrel | Where it costs you |
|---|---|---|---|
| 508 mm (20 in) | Narrow and medium strip, lighter coils, many Asian mills | Smaller barrel, so higher clamping force for the same back tension | Less torque headroom and more bore marking on soft material |
| 610 mm (24 in) | Wide heavy coil from integrated mills | Larger barrel and a longer expansion stroke | Higher machine mass and a wider footprint for the same coil weight |
| 760 mm (30 in) | Very large coils, some aluminium and stainless supply | A long expansion range or interchangeable segments | Either a much longer axial stroke or a second mandrel set, both of which cost money |
| Mixed supply | Job shops buying on price from several mills | One range covering every bore you accept | The widest range drives the design, so the common case pays for the rare one |
Write the range into the specification as measured bore, not nominal bore. "508 mm" is a label; "495 to 520 mm, expansion range 25 mm radial, with 3 mm clearance at each end" is a requirement a supplier can price.
How Much Expansion the Mandrel Really Needs
Expansion range is the difference between the smallest bore you will accept and the largest, plus clearance at both ends. It is a radial figure, and it is the number that decides the mandrel's geometry.
Worked example. Nominal 508 mm, accepted bore 496 to 516 mm. Collapsed diameter must be no more than 496 minus 6 mm of clearance, so 490 mm. Expanded diameter must reach 516 plus 2 mm of bite, so 518 mm.
That gives a radial range of 14 mm, which any four-segment mandrel handles without effort. Change the supply to 508 and 610 mixed, and the same arithmetic produces a radial range of 66 mm.
The stroke follows the wedge angle. For a wedge with an 8 degree half angle, radial expansion equals axial travel multiplied by tan 8 degrees, roughly 0.14.
A 66 mm radial range therefore needs about 470 mm of axial travel.
That single number explains most of the price difference between a standard and a wide-range mandrel.
It is not the segments that cost money; it is the drawbar, the cylinder and the frame length needed to move them 470 mm.
Most suppliers solve the mixed case with interchangeable segment sets instead, which is cheaper to build but adds a changeover.
A segment swap on a 1,250 mm mandrel is a 20 to 40 minute job with two people, so it only makes sense when bore changes are planned weekly rather than per coil.
Where a Small Bore Loads the Mandrel Harder
The mandrel holds the coil by friction between the segments and the bore. Grip force needed rises as the bore gets smaller, because the same torque acts on a shorter lever.
Run the numbers on a 5 tonne coil, outside diameter 1,400 mm, back tension 2.5 kN. Torque at the mandrel is 2.5 kN times the 0.7 m outside radius, so 1.75 kNm.
With a 508 mm bore the barrel radius is 0.254 m. At a friction coefficient of 0.15 between steel segments and steel bore, the normal force required is 1.75 kNm divided by 0.15 times 0.254 m, which is about 46 kN.
Repeat at 610 mm and the radius becomes 0.305 m, so the same torque needs about 38 kN. The smaller bore demands 20 percent more clamping force for identical tension, and that force lands on the bore surface.
Bore marking is the visible result. On aluminium or on thin stainless, 46 kN spread over four narrow segment faces will deform the inner wrap. If the customer inspects the bore after decoiling, that is a defect.
- State the back tension in kN, not as a percentage. Grip force cannot be checked without it.
- Ask for the segment contact area and the resulting bore pressure, not just the rated coil weight.
- For soft material, specify segment pads or a wider contact face before the machine is built, because retrofitting costs more than the option.
Which Mandrel Type Fits the Range You Need
Four designs cover nearly every requirement, and the choice follows directly from the expansion range and the coil weight per unit width.
| Type | Typical radial range | Best fit | Where it limits you |
|---|---|---|---|
| Four-segment wedge | 10 to 25 mm | Single bore, coils up to 10 tonnes | Needs a segment change for a second bore, and grip falls off as the wedge wears |
| Six or eight segment | 20 to 40 mm | Mixed supply with one dominant bore | More parts to maintain and a higher collapsed diameter for the same barrel |
| Long-stroke wedge | 50 to 80 mm | Two bores in regular rotation | Long drawbar and frame, so it costs footprint and money for capacity you rarely use |
| Interchangeable segments | Any, in steps | Three or more bores on a slow rotation | Changeover time of 20 to 40 minutes and a storage and handling requirement |
For a single bore, the simple four-segment design is the right answer and nothing is gained by complexity.
The trade only becomes worth discussing when a second bore appears in more than a few percent of your coil intake.
Rated coil weight and barrel length for each model are published in the coil handling equipment index, and both change the segment count a supplier will quote.
What a Mandrel Cannot Correct
It cannot fix an oval bore. A coil that has sat on a flat floor for a year takes a set, and a mandrel pushed into a 5 mm oval will either jam or force the shape back and mark the inner wraps.
It cannot grip a bore that is larger than the expanded diameter, and no amount of hydraulic pressure changes that.
Oversize bores are usually a winding problem, and the honest answer is to reject the coil rather than run it.
It cannot substitute for correct centring. A mandrel holds the coil on the machine centreline; if the coil is not centred when loaded, the mandrel will hold it off-centre just as firmly.
And the expansion range is fixed at build.
Whatever number you specify is the number you live with for the next decade, which is why the arithmetic above is worth an hour before the order rather than a retrofit after it.
The wider capacity and type decision chain, from coil weight through mandrel to control, is set out in the coil line guide library for coil handling.
Read it before fixing the bore range, because capacity and bore interact.
Can one 508 mm decoiler mandrel accept a 610 mm bore coil?
Only if the expansion range covers it, which means 51 mm of radial travel from the collapsed diameter. Most four-segment mandrels stop at 25 mm, so the answer is usually no.
How much bore variation is normal within one coil?
Three to five millimetres between the inner wrap and the nominal bore is routine, and tight-wound coils can run 8 mm under. Size the collapsed diameter below the smallest bore you will accept.
What back tension can a 508 mm mandrel hold on a 5 tonne coil?
Around 2.5 kN with a 46 kN clamping force at a 0.15 friction coefficient. Push past that and either the coil slips or the bore deforms, depending on the material.
Is a 760 mm bore worth a long-stroke mandrel?
Only above roughly 20 percent of your intake. Below that, interchangeable segments cost less to buy and cost 20 to 40 minutes per change.
Does a larger bore reduce mandrel wear?
It reduces the clamping force needed by about 20 percent for the same torque, which slows segment and wedge wear. It does not remove the need to inspect the wedge annually.
How much clearance should there be between mandrel and bore?
Two to three millimetres radially at the collapsed position is workable. Less than 1.5 mm makes loading sensitive to bore ovality and coil handling damage.
Where to go next
Coil handling is the cluster here, and the chain runs from coil weight to mandrel to control. The companion page takes the same arithmetic through capacity and type selection.
the coil line guide library