How Does EV Battery Tray Stamping Change Coil Feeding?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Sep 23,2026
Summary
A shop that had run steel brackets for four years moved the same servo feeder onto 1.3 mm and 1.6 mm aluminium battery trays and found the job harder, not easier. This follows the first month: the four material properties that broke the steel recipe, the feed roll surface comparison that ended the marking complaints, where the scrap actually came from, and the four conditions under which this setup stops working.
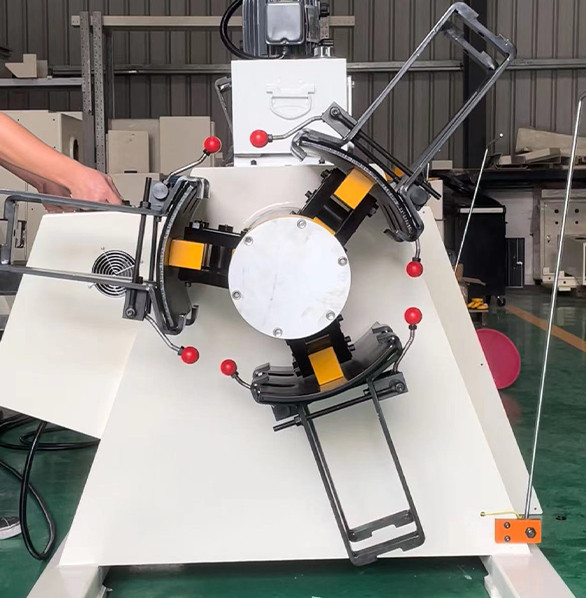
The tray blank is a shallow pan roughly 1,400 mm long, 1.3 mm thick, and it has to sit flat enough that a robot can place cells into it without touching the wall.
That single requirement rewrites most of the feed recipe a shop is used to running on steel.
This is what changed on a customer's NC servo feeder line when they moved from steel brackets to aluminium battery trays, and which of those changes were worth the money.
The measurement framework behind the accuracy numbers is set out in the coil line guide library; the equipment itself is in the product range.
What the Tray Job Looks Like on the Floor
The line runs 5052 aluminium in 1.3 mm and 1.6 mm, coils between 1,200 mm and 1,500 mm wide, at 45 to 60 strokes a minute.
Changeovers between the two thicknesses happen twice a shift. Every tray carries a formed lip and four corner radii, so the die is a shallow-draw progressive with pilot pins.
The plant had been running the same feeder on 1.6 mm SPCC at 90 strokes a minute for four years, and expected the aluminium job to be easier. It was not.
Aluminium is lighter and softer, and both of those properties work against a feed roll that was selected for steel.
Where Aluminium Breaks the Standard Feed Recipe
Four things changed the moment the first aluminium coil went through.
Friction, not force. The coefficient between a hardened steel roll and clean aluminium is roughly a third of what it is against cold-rolled steel.
The old recipe compensated by raising roll pressure, which flattened the strip edge and started marking the surface. Pressure was the wrong lever.
Scratch sensitivity. A mark 0.03 mm deep is invisible on a painted steel bracket and a reject on an anodised tray. Surface finish became a quality characteristic, not a cosmetic one.
Loop behaviour. Aluminium is about a third the density of steel. The same loop depth that stayed stable on steel started hunting on aluminium because the strip weight no longer damped the movement.
Springback in the die. Lower yield means the strip relaxes differently after forming, so pilot pin engagement timing had to move by a few degrees of crank angle.
None of those four are feeder faults. All four are feeder settings.
How Feed Roll Coating Decides Whether You Mark the Tray
The single highest-value change on this line was the feed roll surface, and it cost less than a day of downtime.
| Roll surface | What it gives you on aluminium | Where it costs you | Where it stops working |
|---|---|---|---|
| Hardened steel, smooth | Longest life, cheapest to recondition | Needs high pressure to grip, so it marks soft strip | Anodised or pre-painted surfaces, and any visible panel |
| Hardened steel, knurled | Strong grip at low pressure | Prints a knurl pattern that shows through thin forming | Anything thinner than about 1.2 mm, or visible faces |
| Polyurethane coated | Grip without marking, quiet running | Half the life of steel, and it wears faster on hot strip | Heavy gauge above roughly 2.5 mm, and high line speeds |
| Textured rubber over steel core | Best compromise for 1.0-2.0 mm aluminium | Temperature sensitive, needs a spare set on the shelf | Continuous running above roughly 60 degrees Celsius |
This line moved to a textured rubber surface on the upper roll and a polished steel lower roll.
Roll pressure dropped by roughly 40%, marking complaints stopped, and feed length repeatability actually improved because the strip was no longer being crushed on each stroke.
The spare set sits on the shelf and takes twenty minutes to swap.
Which Line Layout Keeps a 1,500 mm Coil Stable
Wide aluminium coils behave differently from narrow steel coils, and the layout decides how much of that you notice.
Coil width against feeder width. A 1,500 mm coil on a feeder rated to 1,600 mm leaves 50 mm of margin on each side. Edge guides have almost no room to correct tracking before they contact the strip edge.
Distance from pay-off to feed rolls. Keep it short. Every extra metre of unsupported strip is a metre that can bow, twist or pick up a mark from a guide.
Loop support. On 1.3 mm aluminium, a loop that sags into the pit floor will drag and mark. Either shorten the free span or support it.
Entry guide material. Plastic or bronze inserts instead of steel. The guide should never be the hardest thing the strip touches.
Coil car and mandrel. A wider coil concentrates load differently on the mandrel. Confirm the bending rating at that width rather than at the nameplate maximum.
Where the Scrap Actually Came From in the First Month
The plant expected scrap from drawing and cracking. Most of it came from somewhere else entirely.
| Scrap source | Share of first-month scrap | Root cause | What it cost to fix |
|---|---|---|---|
| Surface marking on the tray face | About 45% | Steel feed rolls at steel-level pressure | One roll set, one shift of fitting |
| Feed length drift on thick-to-thin changeover | About 20% | Recipe not recalled with the thickness change | A recipe change in the controller, no hardware |
| Pilot pin marks at the corner radii | About 18% | Pilot release timing still set for steel springback | Two hours of trial with the die setter |
| Edge damage from guide contact | About 12% | Guides set for 1,200 mm left in place on 1,500 mm coils | Guide reset at each changeover |
| Genuine forming defects | About 5% | Draw radius and lubrication, a die issue | Die work, outside the feeder scope |
The pattern is worth reading twice. Roughly 95% of the first-month scrap was traceable to settings and consumables, not to the machine's capability.
Feed accuracy on this line now holds inside plus or minus 0.05 mm at 55 strokes a minute, which is the number the tray gauge actually needs.
Where This Setup Stops Working
A servo feeder with the right rolls handles most tray work. It does not handle all of it, and knowing the edges saves a bad purchase.
- Thickness above roughly 3 mm. Aluminium at 3 mm and above needs feed roll pressure that marks the surface regardless of coating, and the torque margin disappears. At that point a different feeding principle is the answer.
- Widths near the feeder maximum. Running within 20 mm of the rated width leaves no room for edge guides to work. Buy the next frame size instead of the coating upgrade.
- Surface finishes that reject any contact. If the customer inspects a mirror finish under raking light, contact feeding will eventually produce a reject. Ask the question before the machine is ordered, not after.
- High-speed thin gauge. Above about 120 strokes a minute on 1.0 mm aluminium, acceleration limits start to dominate and the accuracy you measured at 55 strokes will not hold.
- Small batch, many alloys. Every alloy change needs a recipe and often a roll check. Below a few hundred parts per setup, the changeover effort outweighs the gain.
With a 45,000 square metre plant and 370 people behind these lines, we would rather say that up front than sell a feeder into a job it cannot hold.
What the Line Looked Like After Ninety Days
Three months in, the numbers had settled and the shop floor had made its own adjustments.
Scrap fell from just over 6% to under 1.8%, and marking complaints stopped entirely once the roll change took effect.
Changeover between 1.3 mm and 1.6 mm dropped from twenty-five minutes to under nine, because the recipe recall replaced a manual re-set of roll gap and pressure.
The operators added two things nobody specified: a plastic-faced guide insert on the entry side, and a laminated card at the machine showing the correct pressure for each thickness.
Neither cost more than a few hundred dollars. Both are the kind of change that only shows up when the people running the line are allowed to own it.
Can one NC servo feeder run 1.3 mm aluminium and 1.6 mm steel?
Yes, with two roll sets and separate recipes. Budget roughly 20 to 40 minutes for the first changeover of each shift and under 10 minutes once the recipes are stored.
Keep the steel rolls off the machine when aluminium is scheduled. Cross-contamination of surface finish is the most common cause of a marking complaint.
Does a battery tray die need ±0.10 mm or ±0.05 mm feed length?
Typically plus or minus 0.10 mm for the tray outline and tighter, around plus or minus 0.05 mm, where pilot pins set the final position.
If the die uses pilots on every station, the feeder only has to land the strip inside the pilot's capture range, which is a considerably easier target.
How much roll pressure is enough on 1.3 mm aluminium?
Start at roughly 60% of the pressure you would use on the same thickness of steel, then increase in small steps until strip slip disappears during a 50-stroke run at production speed.
If you reach steel-level pressure before the slip stops, the problem is the roll surface, not the pressure.
Does aluminium coil need a different mandrel?
Usually not a different mandrel, but a different surface. Aluminium is softer, so segment edges that leave no trace on steel can mark the inner wrap and start a telescope.
Check the bore condition on the first coil and inspect the segments after 20 coils.
At 250,000 parts a year, does a dedicated aluminium line pay back?
When tray production passes roughly 250,000 parts a year and the changeover share exceeds 10% of available run time, a dedicated line usually pays back inside two years.
Below that volume, two roll sets and stored recipes on one feeder are the cheaper answer.
Where to go next
This case turned on feed accuracy holding inside a tolerance band at production speed. The full error budget, from pay-off to die, is worked through in the guide library.
our coil line knowledge base