How Much Drift Does a Loose Servo Feeder Coupling Cause?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 10,2026
Summary
A bracket cell drifted out of tolerance for three weeks while the control reported a perfect feed length. This field case traces 3 percent scrap to 0.15 mm of lash in an elastomer encoder coupling, shows the five checks that isolated it in ninety minutes, and explains why the fault is invisible until the drive reverses under load.
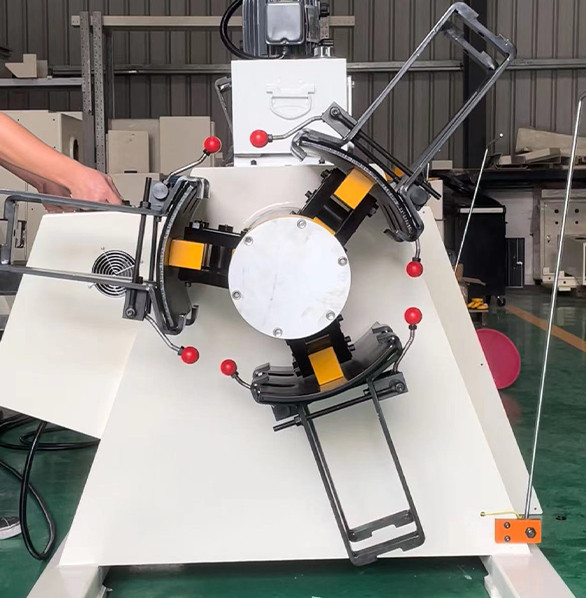
Week one, the scrap rate on a bracket cell moved from 0.6 percent to 0.9 percent. Nobody called maintenance for that.
By week three it was 3.1 percent, and the feed length display had never once shown an error.
This is the account of what a loose encoder coupling does to an NC servo feeder, how it was isolated in ninety minutes, and the cases where the same symptom means something else entirely.
The cell was a standard arrangement: 1.2 mm SPCC, 240 mm feed pitch, a progressive die running at 200 SPM on two shifts.
Nothing exotic. That is what made it useful as a case, because the fault was mechanical rather than electronic, and it hid behind a control that reported perfect health.
The Week the Brackets Started Drifting
The first signal was not a crash or an alarm. It was a slow increase in the number of parts rejected at the final inspection station.
Piercing holes were drifting 0.2 to 0.3 mm off position on roughly one part in forty, always in the feed direction, always late in a run.
Scrap rose in steps: 0.6 percent, then 0.9, then 1.7, then 3.1 by the end of the third week.
Two shifts of operators had adjusted feed length, checked the die, and swapped the pilot pins. Each change held for a few hours and then the drift came back.
What the Operator Saw Before Anyone Measured
The control was reporting the commanded feed length, and the encoder was reporting a position that matched it. Both numbers were stable.
What the operator could see, and the control could not, was a light scuff mark on the strip surface about 30 mm behind the die.
That mark was the roll slipping backwards by a fraction of a millimetre at the end of each feed, as the roll drive reversed to release the strip for the pilot pins.
Once you know to look for it, the scuff is a useful tell. The control sees a clean position because the encoder is measuring the motor, and the motor is doing exactly what it was told.
How the Fault Was Isolated in Ninety Minutes
Five checks took the cell from suspicion to root cause. The order matters, because the cheapest tests come first.
- Measure real pitch against displayed pitch. Mark the strip every hundred strokes and measure with a steel rule. Displayed 240.00 mm, actual 239.72 mm on the drifting parts.
- Run the same cycle dry. With no strip in the rolls the error disappeared completely, which pointed at load-dependent mechanical loss rather than control drift.
- Check roll pressure and surface. Pressure was at specification and the rolls were clean, which removed the most common cause early.
- Feel for backlash at the encoder coupling. With the drive disabled, a dial indicator on the coupling hub showed 0.15 mm of rotational lash.
- Compare with the other axis. The upper roll coupling measured 0.02 mm, which confirmed 0.15 mm as a fault rather than normal wear.
The coupling was an elastomer-spider type with a grub-screw hub. The spider had hardened and taken a set, and the hub had fretted on the shaft.
Under steady torque the lash stayed closed and the position was accurate. At the moment of reversal, the coupling had to take up 0.15 mm of lash before the encoder moved.
What a Loose Coupling Does to the Control Loop
The fault is invisible to the controller because it sits downstream of the measurement, not because the controller is badly designed.
| What the Operator Sees | How a Loose Coupling Behaves | Where Each Diagnosis Costs You |
|---|---|---|
| Displayed feed length correct, parts drift | Lash is taken up after the encoder has already reported position | Chasing it in the control wastes days; the fix is mechanical |
| Drift appears late in a run | Heat softens the elastomer and the lash grows as the cell warms | Thermal compensation in the control hides the symptom and not the cause |
| Scrap in steps rather than a steady line | The lash closes and reopens depending on reversal torque | Operators chase the die, and the die is innocent |
| Error only under load | No strip means no reversal torque, so the lash never opens | A dry cycle that looks perfect sends you looking in the wrong place |
The second row is the one that misleads most teams. Because the error grows with temperature, it looks like a control or compensation problem.
Any fault that appears only after the machine is warm should send someone to the mechanical side with a dial indicator before anyone opens a parameter screen.
Which Failures Look Identical From the Press Side
Four faults produce drift in the feed direction, and they are separated by tests that cost minutes rather than shifts.
| Suspect | How to Confirm It Quickly | Where It Misleads |
|---|---|---|
| Encoder coupling lash | Dial indicator on the coupling hub with the drive disabled | Invisible on screen; only shows under reversal load |
| Roll slip on oily strip | Compare pitch on a degreased sample against production strip | Looks like a coupling fault until you change the material |
| Loose roll-bearing housing | Push the roll axially by hand and watch for movement | Shows as a random error that no parameter change removes |
| Pilot pin wear | Measure pin diameter and compare with the die drawing | Blamed for drift that starts upstream of the die |
Running the four checks in order takes about an hour and settles the question without a specialist.
The Invoice and the Cost of Waiting
The repair was a disc coupling, a keyed hub and four hours of maintenance time. The invoice was small.
The cost of waiting was not. Two extra percent of scrap on a cell producing roughly 12,000 parts an hour at 75 percent utilisation is about 1,080 rejected parts a day.
At a part value of 0.42 USD that is roughly 450 USD a day in material and lost capacity, before the sorting labour that three weeks of drift forced onto the inspection station.
The ninety minutes of planned downtime for the swap cost more than the parts did, and both together still came in under two days of scrap.
Two months later the same cell held plus or minus 0.05 mm on the pitch check, which is the figure the machine was sold against.
Three Configurations That Change the Answer
Three configurations change the picture, and applying the coupling test to them wastes time.
Direct-drive motors. A torque motor mounted straight onto the roll shaft has no coupling to lose its preload, so the same symptom points elsewhere.
Strip-mounted encoders. If position is measured on the strip rather than the motor, coupling lash is compensated automatically and the drift will have a different cause.
Light, slow lines. Below roughly 60 SPM with thin strip, the reversal torque is small and a worn coupling often produces no measurable error at all.
There is a fourth case worth naming.
If the drift appears only on one material and not another, stop testing the machine and look at the strip, because lubricant and surface condition change the answer more than any coupling.
How to Stop It Repeating
Four changes took this failure mode off the maintenance calendar, and none of them cost much.
- Specify a torsionally stiff coupling. A disc or bellows coupling has no elastomer to harden, at a modest cost premium over a spider type.
- Key and clamp the hub. A single grub screw on a round shaft will fret, and fretting is where the lash starts.
- Add a backlash reading to the service schedule. A dial indicator on the hub every 2,000 hours catches it while it is still under 0.05 mm.
- Keep a coupling on the shelf. It is a small part with a long lead time, and a four-hour job becomes a three-day wait without one.
Feeding accuracy is a budget shared across the whole line rather than a single machine number, and the allocation is set out in the coil line guide library.
FANTY builds these machines to hold plus or minus 0.05 mm at 200 SPM, and the coupling specification above is part of how that figure is achieved rather than an optional upgrade.
If you are comparing drive arrangements for a new cell, the coil feeding product range lists the standard configurations and encoder options.
Five questions came out of that week on the shop floor. These are the ones the crew asked most.
Is 0.15 mm of coupling backlash too much?
Measure at the hub. Under 0.05 mm is normal on a healthy coupling; 0.15 mm, as found here, is enough to add 0.3 mm of pitch error at 200 SPM.
Can a worn coupling really cost 2 percent of scrap?
On this cell it cost 2.5 percent, roughly 1,080 parts a day. The size of the loss scales with part value and stroke rate, not with the price of the coupling.
Should encoder couplings be checked every 2,000 hours?
Every 2,000 running hours, or at every annual service. On a two-shift cell that is roughly once a year, and it takes twenty minutes.
Does a coupling fault show up as a random or a repeatable error?
Repeatable but load-dependent. It appears once the cell is warm and under full reversal torque, which is why a dry cycle looks clean.
Is a direct-drive motor worth it above 300 SPM?
It removes one failure mode, not all of them. Direct drive helps most on machines above 300 SPM where reversal torque is highest.
Where to go next
This article sits in the feeding branch of the coil line guide library. It documents one field failure rather than the full accuracy budget behind a line.
Read the feed accuracy error budget