How to Align a Servo Feeder to the Die Centerline
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 28,2026
Summary
A fresh set of pilots lasted nine days because the feed unit sat 0.3 mm off the press centreline, a number nobody had measured since installation. The sequence runs from fixing a permanent datum to proving the result with a strip, with the tolerance for each check and what 0.2 mm of skew does to a pilot bush. It also sets out the four conditions where alignment is not the answer.
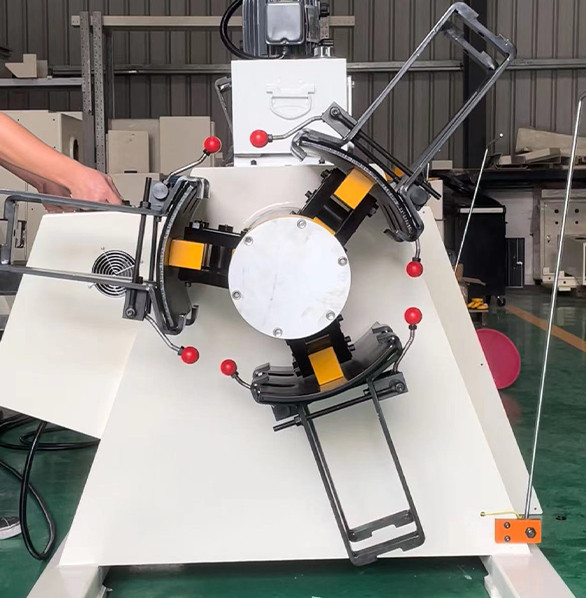
The die came back from the toolroom with a fresh set of pilots and lasted nine days.
The strip was in spec, the feed length was in spec, and the servo feeder was 0.3 mm off the press centreline — a number nobody had measured since the machine was installed.
Alignment is the cheapest accuracy work available to a stamping plant. It costs one shift and a dial indicator, and it removes a wear mechanism that no amount of feed tuning can fix.
What follows is the sequence we use on site, the tolerances worth holding, and the conditions where alignment stops being the answer.
Before You Touch the Feeder: Fix the Datum
Every alignment argument in a press shop comes from two people measuring from two different references. Settle the reference before you touch a bolt.
The datum should be the press, not the die. A die set moves between machines, gets re-shimmed, and is rebuilt with a new bolster plate; the press frame does not move unless something is badly wrong.
Establish the press centreline from the bolster T-slots or from a mandrel bar clamped in the slide, then transfer it to the floor and drill two permanent datum pins.
Those pins are the gift you leave the next maintenance technician. Without them, every future alignment starts from a chalk line and a guess.
Record the numbers you start with. Base level, squareness, pass line height and lateral offset all go on a sheet, dated and signed. Six months later that sheet is the only evidence of what changed.
Take the datum with the die removed. A die set sitting in the press hides the T-slots and pulls the measurement towards whatever shim stack the last job needed.
If the press has been rebuilt or re-levelled since the last alignment, treat the old datum as void. A rebuild moves the slide relative to the bed by a few hundredths, which is the whole tolerance.
Six Steps From Datum to First Good Part
The sequence matters more than the tools. Squaring before levelling leaves you chasing a twist, and setting the pass line before the base is grouted means doing it twice.
- Step 1 — Level the base. Shim to 0.05 mm per metre in both directions, then grout. Check again after the grout cures, because it will move.
- Step 2 — Square to the press. Sweep the feeder's reference face against the press centreline and hold 0.1 mm over 500 mm. This is the number that decides whether the strip runs straight.
- Step 3 — Set the pass line. Match the feeder pass line to the die entry height within 0.2 mm. Higher and the strip lifts the pilots; lower and it drags on the die face.
- Step 4 — Centre laterally. Bring the strip centreline onto the die centreline within 0.5 mm, measured at the die entry rather than at the feeder exit.
- Step 5 — Set the guides. 0.1 to 0.3 mm clearance per side on a 300 mm strip. Tighter guides fight the strip; looser guides let it wander between strokes.
- Step 6 — Prove it with strip. Run twenty strokes and inspect the strip edge for a polished band. A band on one side only means the strip is being pulled sideways.
Budget four to six hours for the six steps on a machine that has never been set up properly. A machine that was aligned last year and has not been moved takes ninety minutes.
What 0.2 mm of Misalignment Does at the Die
Two tenths of a millimetre sounds like nothing on a 300 mm wide strip. The geometry says otherwise once the strip has to travel 400 mm to reach the die.
A 0.2 mm lateral offset over a 400 mm run gives a skew of about 0.03 degrees. Small, but it is applied on every stroke, in the same direction, for the life of the run.
The pilot enters a guide bush with 0.05 mm clearance. A strip held 0.2 mm off centre loads that bush on one side, and the bush wears oval within a few thousand strokes.
The visible symptom is a burr height difference between the two edges of the part. The invisible cost is pilot replacement every quarter instead of every year.
Vertical misalignment is worse than lateral. A pass line 0.5 mm high lifts the strip off the die face, so the pilot drags material instead of locating it.
Feed length then drifts by 0.05 to 0.1 mm without any change to the feed setting at all.
| Check | How to measure it | Tolerance worth holding | Where it costs you |
|---|---|---|---|
| Base level | Precision level, both axes | 0.05 mm/m | Twist shows up as a strip that runs out of square over a long feed |
| Squareness to press | Dial indicator sweep, 500 mm | 0.1 mm | Side load on pilots, oval guide bushes, edge burr |
| Pass line height | Height gauge at die entry | 0.2 mm | Feed length drift of 0.05–0.1 mm, pilot drag marks |
| Lateral centring | Strip edge to die edge, both sides | 0.5 mm | Uneven guide wear, scrap at one edge only |
| Guide clearance | Feeler gauge per side | 0.1–0.3 mm | Too tight scores the edge; too loose lets the strip wander |
The squareness figure is the one to defend. Every other number can drift a little without a visible defect, but 0.1 mm of skew per 500 mm will show up as tool wear within a month.
Read the tolerance as a rate, not an absolute. 0.1 mm over 500 mm is 0.2 mm over a metre, and a 1,300 mm machine measures the full metre whether you intended to or not.
When Alignment Is Not the Answer
Alignment fixes a constant offset. It cannot fix a press that deflects 0.3 mm under load and springs back between strokes, because the error changes with tonnage.
It cannot fix thermal growth either. A 1.2 m steel base moving through a 10 °C shift in a bay with an open door grows about 0.14 mm, and that is larger than the squareness tolerance.
It cannot fix a worn die set. If the guide pins have 0.1 mm of play, the die is moving relative to the press and the feeder is being blamed for it.
Where the measurement misleads. A cold static check says nothing about the machine under load. Check squareness again after an hour of production, with the press at working temperature.
Floor settlement is the slow one. A machine on a slab that was poured thin will drift 0.1 mm a year, which is invisible month to month and obvious over three years.
| Condition | What it does to the feed | What alignment can do about it |
|---|---|---|
| Press deflection under load | 0.1–0.3 mm, varying with tonnage | Nothing; the error changes every stroke |
| Thermal growth, 10 °C shift | About 0.14 mm on a 1.2 m base | Re-check warm, but you cannot remove it |
| Worn die guide pins | Die moves relative to the press | Nothing; rebuild the die set first |
| Thin slab, poor grout | 0.1 mm of drift per year | Re-shim annually, or re-grout |
Bolster wear is the quiet one. A bolster ground 0.05 mm low in the middle tilts every die set that sits on it, and the feed unit gets blamed for a pass line that is only right at the edges.
Put a straight edge and a feeler gauge across the bolster before spending a shift on alignment. Ten minutes there saves a day of chasing a number that cannot be fixed from the machine side.
The Errors That Put You Back at Step One
Aligning to the die instead of the press is the most common mistake, and it produces a machine that is correct for one tool and wrong for the next four.
Measuring with a tape is the second. A tape reads to a millimetre on a good day, and the tolerance here is a tenth of that.
Grouting before checking squareness is the third. Grout moves a base, and a base that was square on shims is often not square after the grout sets.
Forgetting the loop is the fourth. A loop pit that is 50 mm shallow pulls the strip down at the feeder entry and tilts the pass line, which defeats steps three and four at once.
Two operators using two methods will get two numbers from the same machine. Write the method down: instrument, reference face, number of readings, and the speed the check was taken at.
The full error budget from the coil to the die, including how much of the total comes from alignment rather than from the feed itself, is worked through in the coil line guide library.
What follows is what a maintenance planner should be able to answer without calling the supplier.
How much misalignment is acceptable between a servo feeder and the die?
0.1 mm of squareness error over 500 mm, 0.2 mm on pass line height, and 0.5 mm laterally. Anything looser starts loading the pilots instead of the strip.
How long does a six-step alignment take?
Four to six hours on a machine that has never been set up, ninety minutes on a machine aligned within the last year. Grout cure time is additional and usually runs overnight.
Does a 10 °C temperature rise move a 1.2 m feeder base?
By about 0.14 mm, which is more than the 0.1 mm squareness tolerance. That is why a cold alignment has to be re-checked after the press reaches working temperature.
How much side load does 0.2 mm of skew put on a pilot?
Enough to wear a 0.05 mm clearance bush oval within a few thousand strokes. The visible sign is a burr height difference of 0.02–0.05 mm between the two part edges.
Can you align an NC servo feeder to the die instead of the press?
No. The die set moves between machines and gets re-shimmed. Align to the press centreline and let the die sit on its own locating features, or every tool change becomes a realignment.
Where to go next
Alignment is one line in the accuracy budget. The cluster pillar splits the total error between the feed, the strip, the loop and the die, so you can see how much of your tolerance is actually left for the machine.
Read the feed accuracy error budget