What Does a Coil Line Cost to Run Each Year?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 13,2026
Summary
A five-line annual cost model for a coil line: power, rolls and wear parts, spares holding, scrap and downtime. Worked through on a 200 SPM line running 1.2 mm SPCC, where scrap turns out to be five times the power bill. It also sets out which of the five a plant actually controls, the two cases where the arithmetic misleads, and the four terms worth writing into the purchase order.
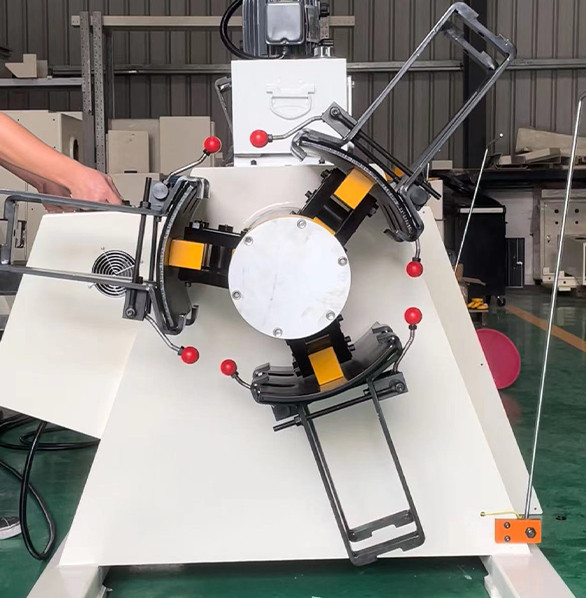
Ask three suppliers what a coil line costs and you get three machine prices. Ask what the line costs to own and the conversation usually goes quiet.
Power, rolls, spares, scrap and unplanned stops all draw on the same budget line. On a two-shift operation they can add 15 to 25 percent to the purchase price within five years.
What follows is an annual running-cost breakdown for an NC straightener feeder line, using figures a plant can check against its own meter and maintenance log.
The Five Costs That Keep Running After Install
Only one of them is on the quotation. The other four arrive in the first twelve months and stay for the life of the line.
Power. A 3-in-1 line with a 22 kW installed load draws roughly 60 percent of nameplate on average, because straightening, feeding and payoff rarely peak together.
Rolls and wear parts. Straightener rolls, feed rolls and the payoff brake pads are consumables. They are the cost most often left out of a five-year budget.
Spares holding. A shelf of servo drives, encoders and hydraulic valves is money that earns nothing. It exists to shorten a stop, not to improve output.
Scrap. Coil-end loss, misfeeds and setup waste are material costs, and material is usually the largest single line in the budget on a line running coated or stainless stock.
Downtime. An hour of stopped press is measured in parts not made, not in kilowatt-hours. It is also the cost that varies most between two plants with identical machines.
| Cost Line | Typical Annual Figure | What Drives It | Where It Costs You |
|---|---|---|---|
| Power | $9,000–$13,000 | Installed kW, duty cycle, hours run | Idle time still draws power, so a line left running between jobs pays twice |
| Rolls and wear parts | $2,500–$6,000 | Strip hardness, coating, tonnage | Hard-chrome and stainless stock shorten roll life sharply; regrind logistics add freight and downtime |
| Spares holding | $4,000–$9,000 | Line criticality, import lead time | Ties up cash and still goes obsolete when a drive series is discontinued |
| Scrap | $6,000–$40,000 | Material price, coil-end loss, misfeeds | Dominate the budget on coated, stainless or high-strength stock |
| Downtime | Site-specific | MTTR, spares on shelf, operator skill | Not a machine cost at all, so it gets attributed to production and never fixed |
Read the table as a ranking of control, not of size. Scrap and downtime are usually the biggest numbers, and they are also the two a plant can move without buying anything.
What the Quotation Leaves Out
Four items show up on almost every installation and on almost no quotation. Budget them before the purchase order, not after the crane arrives.
Foundation and floor preparation. A 3-in-1 line with a coil car needs a level pad and often a recess. Cutting a floor after the machine lands costs far more than designing the pit in.
The power drop and the air supply. Cable, busbar, a dedicated panel and a compressed-air line to the right pressure. Small money against the machine, easy to forget against the schedule.
Training time. Two operators off the floor for a week is a production cost even when the training itself is free. Plan it into a slow month rather than a peak one.
Coil handling outside the line. Storage saddles, a coil car path, and the aisle the forklift needs. A line that feeds perfectly but cannot be loaded efficiently loses its advantage at the loading step.
Running the Numbers on a 200 SPM Line
Take a plant stamping 1.2 mm SPCC on a 200 SPM press, two shifts, 4,000 productive hours a year. Electricity is $0.12 per kWh.
Power. A 22 kW installed load at a 60 percent average duty draws about 13 kW. That is 52,000 kWh, or roughly $6,200 a year at the meter.
Rolls. Straightener rolls on 1.2 mm mild steel typically hold a working profile for 18 to 24 months. A full set reground and refitted lands near $2,800 per cycle, or about $1,600 a year.
Scrap. Coil-end loss on a 5-tonne coil runs 3 to 5 wraps, which is 0.3 to 0.5 percent of the coil. Add setup waste and a realistic figure is 0.8 percent of material value.
At $750 per tonne and 6,000 tonnes a year, 0.8 percent is $36,000. That single line is five times the power bill, which is the point most cost discussions miss.
| Option | Extra Capital | Annual Saving | Where It Costs You |
|---|---|---|---|
| Automatic gap setting | $12,000–$18,000 | $4,000–$7,000 in setup waste | Only pays back above roughly 8 die changes a week; below that it idles |
| Servo payoff with closed-loop tension | $9,000–$14,000 | $3,000–$6,000 in coil-end scrap | Adds a control loop that needs its own tuning and spares |
| Second spare roll set | $2,500–$4,000 | Removes a 3–5 day stop | Capital on a shelf; only justified if the line is a bottleneck |
| Die protection package | $3,000–$6,000 | One avoided die rebuild | Pays back on the first misfeed, or never — it prevents events that do not always happen |
The last row is the honest one. Die protection is insurance, and a plant that has never crashed a die will struggle to justify it on a spreadsheet.
Which Costs You Can Control and Which You Cannot
Split the five cost lines by who actually decides them. That split tells you where to spend management attention.
- Material price and strip hardness: set by the market and the part design, not by the line.
- Setup waste and coil-end loss: fully controllable through gap discipline, loop control and changeover routine.
- Downtime: partly controllable. Spares on the shelf and a written recovery procedure decide the length of a stop, even when the failure itself is random.
A line that holds its gap setting and its coil-end routine will beat a line with better hardware and sloppier habits. That is why two identical machines can carry running costs 30 percent apart.
Where the Cost Model Stops Being Useful
Annual cost models are averages, and averages hide the two cases that matter most. Know them before you quote a number to your finance team.
Low utilisation breaks the arithmetic. A line running 800 hours a year has almost no power or roll cost and a very large fixed cost.
Comparing it to a 4,000-hour line on running cost alone flatters the wrong machine.
Downtime cannot be averaged. One 40-hour failure from a discontinued drive can outweigh three years of smooth running. The model shows the mean and hides the tail, and the tail is what stops the plant.
Scrap figures are not transferable. A 0.8 percent figure from a mild-steel job tells you nothing about a 0.3 mm stainless job with a surface requirement. Rebuild the number for your own material and your own die.
Use the model to compare options on your line, never to predict what a supplier's reference plant achieves. Reference numbers describe their material, their operators and their shift pattern.
Terms Worth Adding to the Purchase Order
Cost control starts in the contract, because the items you cannot price today are the items you will argue about later.
A wear-parts price list, valid for three years. Rolls, brake pads and feed-roll surfaces with fixed prices removes the annual negotiation and the quiet mid-year increase.
A published spare-part lead time. Ask for the lead time on the servo drive, the encoder and the main controller in writing. That number, not the machine price, sets your spares holding.
Energy and air figures at handover. A measured power draw and air consumption at commissioning gives you a baseline. Without it, any later increase is invisible.
MTBF or service history on request. FANTY has 200+ active line installations, and a supplier with that base should be able to tell you what actually fails and how often.
Everything discussed above applies to the line as a whole.
The machine-level specifications that drive these costs are listed on the coil line product range page, and the cost of each spec line is worked through separately.
What does 1 kW of installed load cost per year?
About $290 at 4,000 hours and a 60 percent duty cycle, and about $480 at full duty. Multiply by your installed load before you accept a low-power claim as a saving.
Do straightener rolls really last 18 months?
On 1.2 mm SPCC, 18 to 24 months is typical. On 2 mm HSLA 420 or coated stock, plan on 9 to 12 months, and on stainless the figure can halve again.
Does 1 percent of scrap cost more than the annual power bill?
Almost always. At 6,000 tonnes a year and $750 per tonne, 1 percent is $45,000 against a power bill near $6,000. Fix scrap before you shop for a smaller motor.
Does a 4-hour unplanned stop justify a spare drive on the shelf?
If the imported drive has a 6-week lead time, yes. One avoided 4-hour stop rarely pays for the drive; the avoided 6-week wait usually does.
Is a second roll set worth 3 percent of the machine price?
Only on a bottleneck line. A spare set costs roughly $3,000 and removes a 3 to 5 day regrind stop, which is worth having only if that stop blocks downstream output.
Where to go next
Running cost is one half of the ownership question. The other half is which specification lines you are paying for without needing them, and that mapping sits in the same cluster.