Can a Coil Line Run Electrical Steel Without Damage?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Nov 4,2026
Summary
A motor shop moved a traction-motor family onto a line set up for 1.2 mm mild steel. Three defects appeared in the first shift, and only two of them belonged to the machine. The case covers camber on 0.35 mm NOES, coating damage in the strip path, die clearance for burr, and the 18 percent speed the job actually costs.
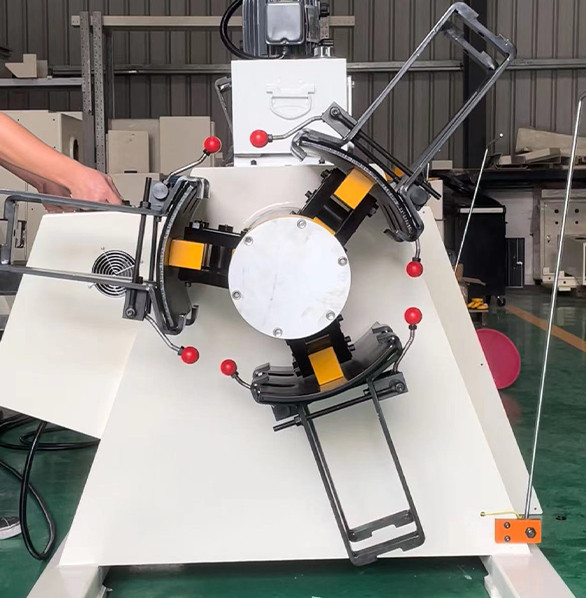
Four hundred kilograms into the first lamination run, the stack height was drifting by 0.15 mm every thousand pieces and the iron loss test had climbed six percent against the sample. Nothing had failed.
The line was simply doing what it was set up to do for mild steel.
Motor laminations are cut from non-oriented electrical steel, usually 0.35 or 0.50 mm thick.
That material carries a 2 to 3 µm insulation coating on each face and enough silicon to work-harden faster than anything on a typical appliance line.
Running it well is a different job from running SPCC.
What the First 400 kg Actually Showed
The customer was a motor shop moving a traction-motor family in house. Material was 0.35 mm NOES, 400 mm wide, coated C5 both sides, and the press ran a three-station lamination die at 220 SPM.
Three defects appeared in the first shift. Camber measured 0.9 mm per metre after the straightener, against a 0.4 mm limit on the drawing. The coating showed bright rub marks along one edge.
Burr on the rotor slots measured 0.06 mm, twice the 0.03 mm the stack drawing allowed.
Each defect had a different owner, which is the part that matters. Two belonged to the line settings, one belonged to the die, and one belonged to nobody until we measured the incoming coil.
Which of the Three Faults Came From the Line
Separate the machine from the material before changing anything. Measure camber on the incoming coil with a straight edge and feeler gauge, then again after the straightener with the same method.
On this job the incoming coil carried 0.5 mm per metre of camber and the straightener added 0.4 mm more. That second number is the diagnostic one: a well-set head reduces camber, it does not create it.
Coating rub marks along one edge pointed at the guide and the edge of the entry roll. Bright, parallel, and confined to 15 mm of the edge is a contact pattern, not a coating defect.
A coating defect from the mill is patchy and follows the rolling direction.
Burr was the die. Slot burr of 0.06 mm on a die that had run 180,000 strokes of 1.2 mm mild steel is a clearance and wear problem, and no line setting removes it.
How Much Straightening 0.35 mm Will Take
Electrical steel has a yield strength in the 350 to 450 MPa range at 0.35 mm, and it work-hardens quickly.
Every extra pass through a roll gap raises yield strength and lowers the magnetic performance the customer is buying.
The instinct on a new material is to add penetration until the strip looks flat.
On 0.35 mm NOES that instinct produces a flat strip that springs back in the die and a core loss figure that fails at the end of the line.
A five-roll head run light is usually enough for mill camber under 1 mm per metre.
Start with penetration at roughly half the value used for 1.0 mm mild steel of the same width, check camber on a surface plate, and stop increasing as soon as it comes inside the drawing limit.
If camber still exceeds the limit at that setting, the coil is the problem. Over-straightening a bad coil buys a flat strip today and a rejected stack next month.
Where the Coating Fails Before the Die Does
The insulation layer is 2 to 3 µm per side and it is the only thing preventing interlaminar shorts in the finished stack.
A rub mark that reaches bare steel costs more than a dimensional deviation, because it shows up as heat in the motor, not as a reject at the press.
Four contact points do most of the damage: the entry guide, the edge of the first straightener roll, the feed rolls, and any fixed stripper or wiper the strip drags across.
Hardened steel rolls with a polished finish are the usual cause on the last two.
| Change | What it buys | Where the trade bites |
|---|---|---|
| Polyurethane or coated feed rolls | Grip without marking the C5 surface | Shorter roll life and a re-coating interval measured in months, not years |
| Reduced roll pressure on the feed unit | Fewer edge rub marks | More slip risk on oily strip, so feed length has to be monitored, not assumed |
| Roller guides instead of fixed guides | No sliding contact on the strip edge | Extra setup time per width change and one more wear item |
| Dedicated slitting before the line | Clean, burr-controlled edge from a known source | An added process step and a second handling risk on 0.35 mm material |
Cleaning matters as much as roll material. A single chip embedded in a feed roll will mark every metre that passes it, and on coated material that mark is permanent.
Roll hardness and surface finish are usually stated on the build sheet rather than the quotation.
The product specification library shows the standard roll materials offered, which is a faster starting point than asking the question twice.
What This Kind of Line Still Cannot Do
It cannot anneal. Punching stress raises core loss, and a stress-relief anneal at 750 to 800 °C is what recovers it. A coil line delivers flat, accurate blanks; it does not deliver magnetic properties.
It cannot hold 0.03 mm burr with a worn die. Burr is a die clearance and sharpness question, and the line only decides whether the strip arrives square and flat enough for the die to do its job.
It cannot compensate for a coil with bad edge quality. Slit edge burr above 0.02 mm on the incoming coil propagates through the stack no matter how the rolls are set.
And it cannot run 0.35 mm at the same speed as 1.2 mm without a decision.
Higher speed means more slip in the feed rolls and more marking on coated material, so throughput is traded against surface quality rather than maximised.
What Changed on the Second Run
The straightener went to a light five-roll setting and camber came in at 0.3 mm per metre. Feed roll pressure dropped one step and the edge rub disappeared within 200 strokes.
The die was resharpened and clearance reset to 6 percent of thickness, which brought slot burr to 0.025 mm.
A roller guide replaced the fixed entry guide on the operator side, and the line gained a mandatory roll wipe at every coil change.
- Straightener penetration cut to roughly half the mild-steel value, which took camber from 0.9 to 0.3 mm per metre.
- Feed roll pressure down one step and a roller guide on the operator side, which removed the edge rub within 200 strokes.
- Die clearance reset to 6 percent of thickness after resharpening, which brought slot burr from 0.06 to 0.025 mm.
Speed settled at 180 SPM for 0.35 mm against 220 SPM for the 0.50 mm family.
That 18 percent throughput loss was accepted because the alternative was a coating defect rate that showed up as motor temperature rise three months later.
The press now holds ±0.05 mm feed length over a full coil, which is what the stack tolerance needs. The line had always been capable of that; the setup had not been asking for it.
How to Check a Line Before You Quote Laminations
Run these five checks on the machine you already have before promising a lamination job. Each one is cheap, and each one has sunk a quotation in the past.
- Measure incoming camber on three coils from three lots. Anything above 1 mm per metre needs a material conversation, not a machine setting.
- Confirm the feed rolls are polymer or coated. Hardened steel rolls mark C5 coating on the first coil.
- Check die clearance against 5 to 7 percent of thickness and inspect sharpness, because burr is decided there.
- Verify that every guide and wiper in the strip path is either rolling or non-contact. Fixed guides are a marking source.
- Ask whether the customer's drawing is a burr and camber spec or a core loss spec. If it is core loss, the anneal belongs in the process, not on the machine.
Flatness and camber limits for coated and thin material are covered in more detail by the coil line guide library, including the roll-count geometry that decides how much correction a given head can deliver.
Does a 0.35 mm electrical steel coil need a different feed roll pressure?
Usually one step lower than 0.8 to 1.2 mm mild steel, because the coating marks before the roll slips. Watch feed length for the first 50 strokes after any pressure change.
What burr height is acceptable on a motor lamination?
0.03 mm is a common drawing limit and 0.02 mm is better for stacked rotors. Above 0.05 mm the interlaminar gap starts to affect core loss measurably.
How much speed does lamination work cost compared with mild steel?
Expect 15 to 20 percent, for example 180 SPM instead of 220 SPM on the same press. The loss comes from slip control and coating protection, not from the machine's rated speed.
Can a stress-relief anneal be skipped if the burr is under 0.03 mm?
Only if the drawing is dimensional. Punching raises core loss regardless of burr, so a magnetic specification needs the anneal even on a clean cut.
Is one coil line enough for both 0.35 mm and 0.50 mm families?
Yes, with two saved recipes. The difference is penetration depth, roll pressure and top speed, and all three should change together rather than one at a time.
Where to go next
Thin coated material exposes every contact point in the strip path, which is the subject of this cluster. The companion page works through the roll geometry behind the camber figures above.
our coil line knowledge base