Can an NC Straightener Feeder Do a Leveler's Job?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 14,2026
Summary
Flatness in I-units decides the machine class before any supplier is involved. This comparison works a 0.8 mm SPCC coil at 200 SPM through both options, shows where a 7-roll straightener head stops reaching the spec, and names the four situations where the comparison itself stops being useful.
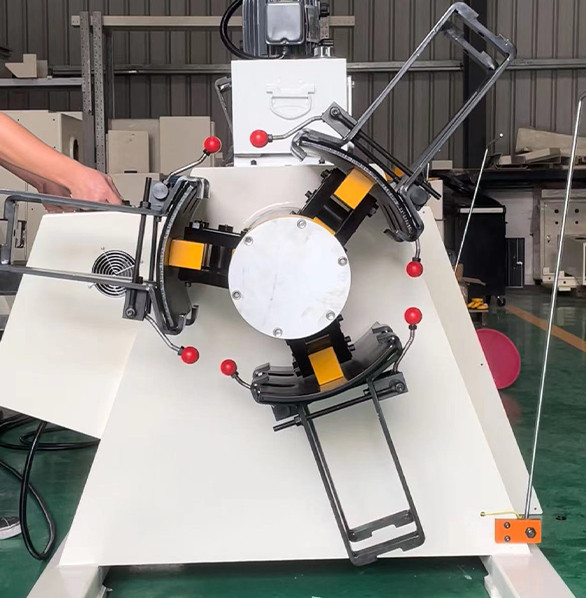
Buyers ask this question in the wrong order. A precision leveler and an NC straightener feeder both take curvature out of strip, so they look like alternatives on a quotation. They are not.
One removes coil set and gross shape at production speed, the other chases a flatness number that the first machine cannot reach. The right choice comes from the spec, not from the machine list.
Start From the Flatness Spec, Not the Machine Name
Flatness on steel strip is measured in I-units, and the number on the drawing tells you which machine class you need before any supplier gets involved.
A general stamping job usually carries a flatness requirement around 25 to 40 I-units. A visible panel or a part that will be laser cut or welded often carries 8 to 12 I-units.
Those two bands do not overlap. A 7-roll straightener head with 60 mm rolls will hold the first band comfortably at 200 SPM. It will not hold the second, at any speed.
So the first decision is arithmetic. Write the I-unit figure on the enquiry sheet and the machine choice narrows immediately.
How the Two Roll Trains Differ
The difference is not roll count. It is roll diameter, penetration depth and the tension applied across the roll train.
| Configuration | What It Gives the Run | Where It Costs You |
|---|---|---|
| 3-in-1 straightener feeder alone | Coil set and gross shape removed at line speed; one operator, one footprint | Flatness bottoms out around 20 I-units; thin strip still shows waves |
| Straightener feeder plus in-line precision leveler | Holds 8 to 12 I-units on 0.5 to 1.5 mm strip | Extra machine, extra floor length, and a second setup to maintain |
| Offline leveler before the coil line | Flatness fixed once, then fed as normal coil | Double handling, an extra coil movement, and a cut-to-length step |
| Leveler with tension bridle | Highest flatness on thin, wide strip | Slowest of the four; the bridle itself needs maintenance |
A straightener head of 7 to 9 rolls at 60 to 75 mm diameter carries a penetration of 1.5 to 2.5 mm on 1.0 mm strip. That is enough to yield the outer fibres and erase coil set.
A precision leveler uses 17 to 21 rolls at 20 to 30 mm diameter with a penetration measured in tenths of a millimetre, working the strip repeatedly at low strain. Small rolls, many passes.
That geometry sets the thickness window. Leveler rolls are too small to work 3 mm strip, while a straightener head with large rolls cannot put in the fine, shallow work that fixes edge wave.
The Flatness Number That Decides the Choice
Take a 1,250 mm wide, 0.8 mm SPCC coil on a 200 SPM line. Coil set is obvious and the drawing asks for 20 I-units.
A straightener feeder with a 7-roll head handles it. Feed length holds at ±0.05 mm, the strip enters the die flat enough, and the part meets the drawing after forming.
Change one input and the answer flips. Same coil, same thickness, but the customer now specifies 10 I-units because the panel is visible on the finished product.
The straightener head runs out of travel. Penetration deep enough to reach 10 I-units would mark the surface and start to narrow the strip, so the operator backs off and the flatness number misses.
Add a precision leveler in line and the same coil reaches 8 to 10 I-units. The cost is a second machine, roughly 2 metres of extra line length and another setup to hold.
| Coil and Spec | Straightener Feeder Alone | With a Precision Leveler In Line | What the Extra Machine Costs You |
|---|---|---|---|
| 1.2 mm SPCC, 25 I-units | Holds the spec | Not needed | A machine that sits idle on most jobs |
| 0.8 mm SPCC, 20 I-units | Holds at 200 SPM | Holds with margin | 2 metres of floor and a second setup to maintain |
| 0.8 mm SPCC, 10 I-units | Misses by 10 to 15 I-units | Reaches 8 to 10 I-units | Line speed falls to roughly 120 SPM |
| 0.5 mm pre-painted, 12 I-units | Marks the surface at the penetration needed | Reaches the spec but can still mark | Surface risk on both machines |
| 3.0 mm HR, 30 I-units | Holds the spec | Rolls too small to work the strip | No benefit at all for the money spent |
When the Straightener Feeder Is the Right Answer
Most coil lines we ship never need a leveler, and the reasons are practical rather than commercial.
Thick material. Above about 2.5 mm the leveler roll geometry stops being effective, and the straightener head is the only machine that can bend the strip far enough to yield it.
Die-side correction. If the part is formed in a die that straightens the blank in the first station, flatness measured at the coil is not the controlling number.
Speed. A 3-in-1 NC straightener feeder feeds at 200 SPM. An in-line precision leveler on the same strip typically runs slower, and on a high-volume line that difference shows in the output figures.
Footprint. A combined decoiler, straightener and feeder occupies roughly half the floor length of the same function split across separate machines. That saving is a real cost advantage, not a marketing line.
More than 200 of these combined lines are in the field, and the pattern is consistent.
The plants that chose a straightener feeder alone did so because the flatness spec allowed it, not because the budget forced it.
The five questions below are the ones that actually separate the two options in a quotation review.
Can a 7-roll straightener feeder reach 10 I-units on 0.8 mm strip?
Not reliably. Expect 20 to 25 I-units at production speed. Reaching 10 I-units on 0.8 mm normally needs a leveler with 17 rolls or more.
At what thickness does a precision leveler stop working?
Above roughly 2.5 to 3 mm. The roll diameter needed to work thick strip is larger than a leveler roll train can carry, so the job moves back to a straightener head.
How much line length does an in-line leveler add?
Around 2 to 2.5 metres including the loop between machines. That is often the deciding factor in a plant with no spare bay length.
Does a leveler fix camber as well as flatness?
It reduces camber but does not remove it. Camber comes from a width-wise difference in length, and the straightener or leveler can only redistribute so much of it.
Is a 3-in-1 straightener feeder cheaper than a separate leveler line?
On a like-for-like function, yes, by a wide margin. One machine replaces three, and the floor length saving is usually larger than the price saving.
Four Checks That Separate the Two Quotes
When two suppliers quote different machine classes for the same part, four checks settle it without a trial run.
- Ask for the flatness figure in I-units at a stated strip tension, not as a range
- Ask what thickness range the roll train was sized for, not what it can pass
- Ask for the line speed at which the flatness figure was measured
- Ask which machine carries the setup responsibility when both are installed in line
The third item catches most of the gap between quotes. A flatness figure measured at 40 SPM is not the same claim as one measured at 200 SPM.
The fourth item matters once both machines are on the floor. If the leveler holds flatness and the straightener head holds feed length, someone has to own the interaction between them.
Ask the same four questions of both suppliers and the comparison becomes arithmetic rather than opinion.
Where the Comparison Stops Being Useful
Framing this as a straight choice between two machines breaks down in four situations, and in each of them the flatness number is the wrong thing to optimise.
When the flatness fault is in the die. A part that comes out twisted after forming has a tooling problem. No upstream machine fixes a die that is not level.
When surface quality is the constraint. A leveler works strip many times at low strain and can leave fine marks on pre-painted or polished material. On that strip the flatter machine is the wrong machine.
When the coil supplier changes. A flatness recipe tuned to one mill's strip will not transfer unchanged to another mill's. Both machines need re-verification on a new supply.
When throughput is the real limit. On a line that must run at 200 SPM continuously, adding a slower machine in line reduces output more than the flatness gain is worth.
One measurement trap remains. I-unit figures quoted by different suppliers are not always taken at the same strip tension.
Compare readings taken under the same back tension, or the numbers are not comparable at all.
CE-certified and shipped into more than 60 countries, these lines are specified on the flatness figure the customer actually measures, not on a catalogue claim.
The full flatness chain, from roll count to penetration, is set out in the flatness cluster of our 3-in-1 decoiler straightener feeder guide.
Two Numbers to Put on the Enquiry
An enquiry that carries a flatness figure in I-units and a thickness range will get comparable quotes. An enquiry that asks for a machine will not.
Add the strip tension at which the flatness will be measured. Without it, two suppliers can quote the same I-unit target and mean different things.
State the maximum width and the coil weight as well. On a 1,250 mm coil at 5 tonnes, roll deflection starts to matter, and roll diameter has to be chosen for the load rather than for the thickness.
With those four values on the sheet, the choice between a straightener feeder and a precision leveler is usually decided in the first meeting rather than the third.
Where to go next
Flatness, roll geometry and penetration form one cluster in our coil line knowledge base. This article sits under it, one layer below the specification overview.
The Coil Line Guide Library