How to Run a Welded Joint on an NC Straightener Feeder
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Nov 17,2026
Summary
A weld bead standing 0.4 mm proud is 20 percent of a 2 mm strip arriving at a gap set 0.05 mm under, and the roll absorbs the difference. This article covers joint detection, what each joint type does to the roll stack, a five-step pass sequence with the gap, speed and tension figures for each, and the part count to divert at the die. It names four joints that should not be run at all and the four fields worth logging afterwards.
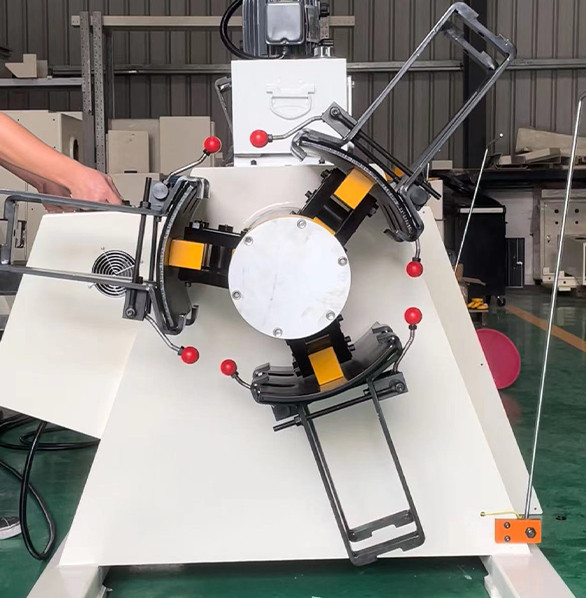
A welded joint is the only place where the strip gets thicker mid-run. On 2.0 mm CR a bead stands 0.3 to 0.5 mm proud.
That is 15 to 25 percent of the material thickness arriving at a roll gap set 0.05 mm under.
Run it at line speed and something has to absorb that. Usually it is the roll surface, and the mark it leaves repeats for the rest of the coil.
This is the sequence we teach operators for a joint pass, and the joints that should never be run.
How to Spot the Joint Before It Reaches the Rolls
Detection is the whole job. A joint that reaches the roll stack unnoticed costs a roll re-cover; one that is caught thirty seconds earlier costs a slow pass.
On an NC straightener feeder the joint meets the entry pinch roll before anything else, so that is where detection has to start.
Three methods exist, and most lines use the weakest one.
A weld detector is a non-contact sensor that reads a thickness step or a magnetic change. It costs USD 900 to 2,500 and works on any material, including stainless.
A length counter compares metres run against the recorded coil length. It is free and it catches the joint on any coil that was welded to a known length.
An operator mark is a chalk line or a flag at the coil entry. It works until the operator is on a break.
Fit the detector if the line runs above 100 SPM, and keep the counter as the backup. The counter is also what tells you the joint is 4 m away rather than 40.
What the Bead Does to a 0.05 mm Roll Gap
A roll gap is set to the strip thickness minus a small penetration. On 2.0 mm CR that is usually 1.95 mm.
A butt weld with the bead left on presents 2.35 mm to that gap. The roll cannot open, so the machine frame, the roll neck and the strip all deflect to make room.
The result is a pressure spike that flattens the bead into the roll surface, and a witness mark that transfers to every part until the roll is polished.
Weld hardness makes it worse. A flash weld in CR runs 1.4 to 1.8 times the base hardness, so the bead resists flattening and takes the load on a narrow band.
| Joint type | What it leaves on the strip | How it behaves in the roll stack | Where it costs you |
|---|---|---|---|
| Flash butt weld, bead ground flush | Hardness band 10 to 30 mm wide | Passes at reduced speed with a small gap lift | 20 minutes of grinding per joint |
| Flash butt weld, bead left on | 0.3 to 0.5 mm proud on both faces | Roll marking, and a gap that cannot open fast enough | A roll polish, or a re-cover if it repeats |
| Lap weld | A step of one material thickness | Acts like a 2 mm shim through the rolls | Two thicknesses of strip to scrap, not one |
| Stapled or tabbed joint | Local hard spots, no bead | Passes, but the tab can catch a wiper or a guide | A jam at the entry, and a torn edge behind it |
Only the first row belongs in a line running above 80 SPM. The rest are decisions made upstream, at the welder.
The Pass Sequence, Step by Step
Five steps, in this order. Skipping the third one is the most common mistake we see on a shop floor.
- Stop the line with the joint 1.5 m before the entry pinch roll, not at the roll.
- Open the roll gap by the bead height plus 0.10 mm, and write the figure on the setup card.
- Release the hold-down and reduce back tension to about 30 percent of the running value.
- Run the pass at 50 percent of line speed, and do not change speed while the joint is in the rolls.
- Restore gap, tension and speed only after the joint is past the last roll, then re-check the first part.
The third step is the one operators skip, because the hold-down feels unrelated to a thickness change. It is not: a hold-down pressing on a 0.4 mm bead adds the load that marks the roll.
| Parameter | Normal run | Joint pass | What the change costs you |
|---|---|---|---|
| Roll gap | 1.95 mm | 2.25 mm | Two or three parts out of flatness tolerance |
| Line speed | 120 SPM | 60 SPM | About 40 seconds per joint |
| Back tension | 8 MPa | 2.5 MPa | The coil can loosen on the mandrel |
| Hold-down | On | Released | The strip can lift at the entry |
Every row trades a part or a second against a roll surface. On a line running 40 coils a day, that is 40 joint passes a day, so the trade is worth calculating rather than guessing.
What Changes at the Die End
The joint does not stop being a problem when it leaves the rolls. It arrives at the die with a hardness band, a thickness step and, often, a slight bend.
Count three to five parts to scrap on either side of the joint. The exact number depends on the die pitch and how much of the bead survived the pass.
If the die uses pilots, the joint will resist them. A pilot entering a hole punched through weld metal can shear, and that failure usually takes the die down for a day.
Set the counter to divert those parts at the chute rather than trusting the operator to catch them. Manual sorting works until the shift when it does not.
If the part is visible in the finished assembly, check the first good part after the joint for a witness mark before the line returns to full speed.
A joint also disturbs the loop. Where the line runs a loop pit, the thicker section can jump the rollers, and the dancer then over-corrects for a metre or two.
Which Joints Should Not Be Run at All
A lap weld on strip under 1.0 mm. The step is one full thickness, which no gap lift can absorb without losing the pass entirely.
A bead that has not been ground and a die that needs 0.03 mm flatness. The two requirements are incompatible, and the roll will lose.
A joint in high-strength material above 600 MPa yield. The weld zone is brittle, and a roll stack with any penetration at all will crack it. The crack then runs into the part.
A joint on a line with no detector and no counter. This is not a material limit, it is a process limit, and it is the one that produces the expensive failures.
Those four cases are worth writing into the work instruction, because each one is decided before the coil reaches the machine.
What to Log After Each Joint
A joint log turns a recurring cost into a trend you can act on. Four fields are enough.
Record the coil number, the joint type, the gap used, and whether a mark appeared on the first good part.
After twenty joints the pattern is obvious. If marks cluster on one material supplier, the argument moves to the coil order. If they cluster on one shift, it moves to training.
That is the difference between replacing rolls twice a year and replacing them twice a quarter, and it costs one line in a notebook.
Two joints in a row from the same coil is a different signal. It usually means the coil was built from several short lengths, and the mill should hear about it.
Roll marking from a joint is a gap and penetration question before it is a roll quality question.
The 3-in-1 decoiler straightener feeder roll geometry is set out in the flatness pillar, for anyone sizing the stack around it.
What to Write Into the Setup Sheet
The setup sheet is what the next operator reads at 3 a.m., and a joint pass is exactly the procedure that gets lost between shifts.
Put the gap figure in millimetres, not as "open slightly". Put the speed as a number, not as "slow".
Add the reject count and the position of the first part to check. Add the joint type the welder is set to produce.
A sheet with those four numbers removes the argument about whether the last mark came from the joint or from the coil, which is the argument that costs the most time.
The equipment data library lists roll diameters and gap ranges by model, so the joint-pass figure can be written as an offset rather than a fixed number.
How much gap lift does a 0.4 mm weld bead need on 2 mm strip?
Open to 2.25 mm, which is bead height plus 0.10 mm. Less than that and the bead takes load on a narrow band and marks the roll.
How many parts should be scrapped around a joint?
Three to five, depending on die pitch. At a 200 mm pitch, five parts covers 1 m of strip on either side of the weld.
At what line speed can a bead be run without lifting the gap?
Below 40 SPM on 2 mm CR, and only with a ground bead. Above that, the load spike arrives faster than the roll can deflect.
Does a 0.05 mm roll mark matter on a painted part?
Yes. A 0.05 mm witness mark shows through a 60 micron paint film as a visible line, and it repeats every roll revolution for the rest of the coil.
How long does a joint pass take on a 120 SPM line?
About 40 seconds of lost output, plus 30 seconds to restore settings. Forty joints a day is 45 minutes of production, which is the real cost of the procedure.
Where to go next
A joint pass is one exception to a roll setting that has to be right for the other 99 percent of the coil. The cluster's flatness pillar explains how that setting is derived from roll count, pitch and penetration.
Read the flatness and roll setting pillar