What Happens When a Feeder Is Sized on Press Tonnage?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 17,2026
Summary
The order went out as a 200-ton press, so the feeder was picked to match. It ran fine for four months, then a thin-gauge job exposed short feeds that no amount of tuning could remove.
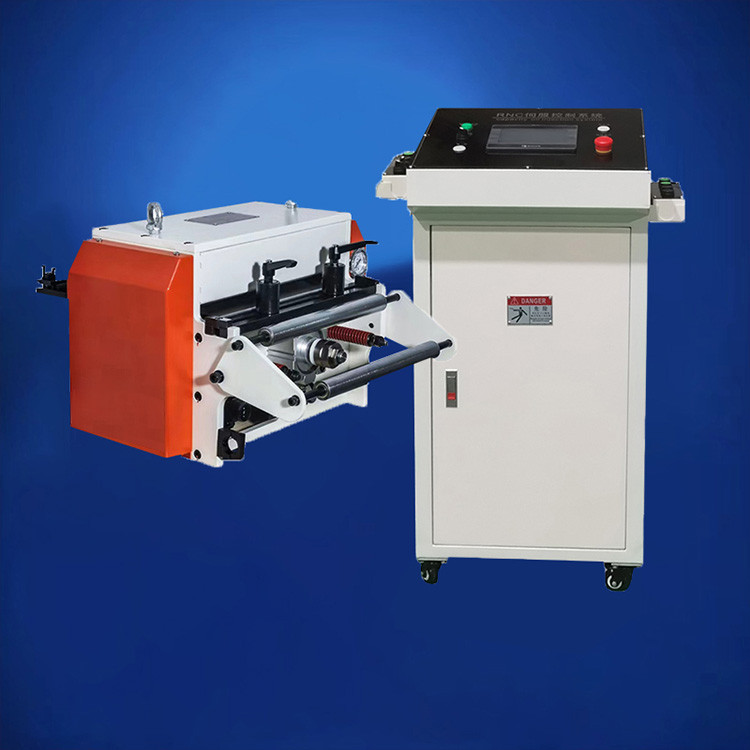
A tier-two stamping plant in the Midwest ordered a press, then ordered a coil feeder to go with it. The purchasing note said 200-ton press, and the feeder quotation came back sized to match.
Nothing about that sequence is unusual. It is how a large share of feeder orders still get written.
Four months later the plant was rejecting 6 percent of a thin-gauge job and could not explain why. The story of finding the answer is more useful than the answer itself.
The Order That Started With a Tonnage Number
Tonnage describes the press, not the strip. It says how hard the press can push, and nothing about what the feeder has to pull.
The plant's job mix at the time of purchase was 2.0 mm and 2.5 mm mild steel, 900 to 1,200 mm wide. Any feeder in the catalogue would have run that work.
The quotation was written against a 200-ton frame, which produced a feeder with generous roll diameter, a wide body and a motor sized for the heaviest strip that frame could handle.
On the original job mix the machine was, if anything, overbuilt. It fed accurately, it never slipped, and the maintenance log stayed empty.
Month One: It Ran and Nobody Complained
Commissioning took a day and a half. Feed length calibration was straightforward and the first production run held 0.08 mm over 300 strokes.
The operator liked it because the rolls gripped hard and nothing moved. Roll pressure was set high at commissioning and never touched again.
For four months the feeder ran two shifts on 2.0 mm and 2.5 mm work with no quality escapes. It became the machine nobody thought about, which is the best thing you can say about a feeder.
Month Four: Short Feeds on the Thin Gauge Job
The plant won a contract for 0.6 mm galvanised panels, 700 mm wide, at 180 SPM. First shift produced 40 good parts, then a run of short feeds averaging 0.4 mm.
The die survived because the pilot pins were doing their job. The scrap bin did not.
The obvious suspects were ruled out one by one: encoder coupling was tight, feed length was correct for the die, and the drive reported no following error.
Roll pressure was still set for 2.5 mm material. On 0.6 mm strip that pressure flattened the strip section under the roll, and the roll recovered before the strip did.
The material was being extruded slightly at every stroke, and the accumulated effect over 200 strokes showed up as drift rather than as a single bad feed.
Reading the Data Backwards
The plant pulled 200 strokes of feed length data and plotted it as cumulative error rather than absolute error. The picture changed immediately.
Absolute error per stroke looked random and small, well inside tolerance. Cumulative error climbed steadily and crossed the die's pilot clearance at around stroke 140.
That pattern points at either roll slip or material deformation, and both were happening: high pressure on thin strip causes the second, which causes the first.
A single-stroke check would have passed this machine every day of the week. Only the accumulated run exposed it.
What the Sizing Sheet Should Have Asked
| Sizing input | What the order said | What it should have said | What It Costs You if Wrong |
|---|---|---|---|
| Strip section | 2.0 to 2.5 mm | 0.6 to 2.5 mm | Roll pressure and roll diameter both wrong for the thin end |
| Yield strength | Not stated | 250 to 340 MPa range | Grip force margin wasted or missing |
| Feed length range | Not stated | 80 to 400 mm | Acceleration profile tuned for the wrong duty |
| Line speed | 180 SPM nominal | 180 SPM sustained at 0.6 mm | Motor and drive sized on the wrong load case |
| Coil weight | 4,500 kg | 4,500 kg, 508 and 610 mm bore | Not a feeder issue, but it changes line dynamics |
Tonnage appears nowhere on that list. It is a useful number for the press foundation and a misleading one for the feeder.
The Fix and What It Cost
The fix was a pressure regulator with a gauge readable at a glance, plus a pressure table for each gauge in the job mix.
Total parts cost was under USD 900. The commissioning engineer spent two hours setting four pressure values and writing them on a laminated card taped to the guard.
The scrap and rework from four months of intermittent short feeds was never fully calculated, but the quality engineer put the known figure above USD 30,000.
Nothing was replaced. The machine was correctly built and wrongly set, which is the usual shape of this particular failure.
| Cost item | What it was | What it cost | What It Bought You |
|---|---|---|---|
| Pressure regulator and gauge | Single panel-mounted unit | USD 420 | Readable pressure at the machine |
| Fitting and labour | Two hours, plant fitter | USD 380 | No production downtime |
| Commissioning visit | Two hours, supplier engineer | USD 900 | Four pressure values and a laminated card |
| Scrap during the fault | Four months, intermittent | USD 30,000 estimated | Nothing. This is the price of the sizing error |
| Customer return risk | Not triggered | Not triggered | Would have doubled the total |
The table is lopsided on purpose. Almost all the money sits in the row that bought nothing at all.
That is the shape of most sizing errors. The correction is cheap and the exposure before correction is not, which makes the case for a proper sizing sheet financial rather than technical.
The plant now writes a thickness range on every feeder enquiry, including repeat orders for machines they already own and understand.
A second machine bought on the same tonnage logic would have repeated the same four months on a different press.
Sizing Rules That Survive a Job Mix
For reference, the press feeder range publishes roll diameter, feed length and motor rating per model, which is exactly the comparison a sizing sheet needs.
Reading that sheet against a job mix takes an afternoon. Buying the wrong size takes a year to notice and four months to admit.
- Size on the lightest strip in the range, not the heaviest. Light strip exposes grip and pressure limits that heavy strip hides.
- State the full thickness range with yield strength, and treat any future material as a new sizing exercise.
- Ask for a pressure-versus-gauge table at commissioning, and require it to be posted at the machine.
- Test at the fastest speed and thinnest material together, because that combination is the worst case and also the one nobody tests.
- Log cumulative feed error, not single-stroke error. The die cares about accumulation.
Where Tonnage Is Still a Useful Number
Tonnage belongs in the press specification, the foundation design and the die load calculation. It is a legitimate input in all three.
It also correlates loosely with feeder size in practice, because bigger presses tend to run wider and heavier strip. That correlation is not a sizing method.
What tonnage does tell you is die weight and shut height, both of which constrain where the feeder can sit.
It also sizes the press foundation, which matters when a line has to fit an existing bay without rebuilding the floor.
Those are real constraints. They are simply not the ones that decide whether strip slips between two rolls at 180 SPM.
A sizing sheet that starts at tonnage and ends at roll pressure is working backwards through the problem, and it will produce a machine that runs until the job mix moves.
The failure mode above is what happens when a correlation gets used as a specification. It works until the job mix changes, and job mixes always change.
Where to go next
Feeder sizing is one link in the chain that ends at the die. The error budget from decoiler to die shows how each element's tolerance adds up, and it is the page to read before signing a sizing sheet.
The Coil Line Guide LibraryDoes a 200-ton press need a 200-ton-rated feeder?
No. Feeder capacity follows strip section, feed length and speed. A 200-ton press can run 0.6 mm strip that any 2-ton-capacity feeder would handle.
How much feed error is acceptable over 200 strokes?
Under 0.10 mm accumulated for most progressive dies. Above that, pilot clearance starts to be consumed and the die marks the strip.
Why does high roll pressure cause short feeds on thin strip?
The roll flattens the strip section locally, the strip springs back behind the roll, and grip is lost for a fraction of the stroke. The error accumulates rather than appearing once.
What does a pressure regulator with a gauge cost?
Under USD 900 for most press feeder sizes, including fitting. It is the cheapest fix in this article and the one most often skipped.
Can cumulative feed error be corrected in the controller?
Partly. Compensation helps, but it masks a mechanical cause. Fix grip and pressure first, then compensate for what remains.