Why Does a Straightener Mark the Strip Every Roll Turn?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Nov 19,2026
Summary
A faint line every 322 mm on 1.2 mm strip pointed to a 102 mm work roll, and two shifts of gap changes had made it worse. The article shows how to measure the pitch, the circumference table that names the roll, the tests that separate four causes, and the repairs worth doing.
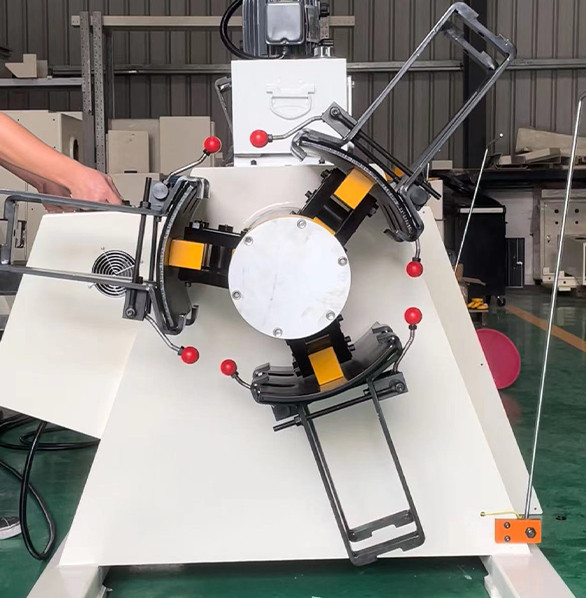
A mark that repeats at a fixed pitch is a roll defect, not a setting problem, and the pitch itself names the roll.
An appliance panel job on a 5-roll NC straightener feeder produced a faint line every 322 mm along 1.2 mm SPCC. The line was 8 mm long, on the top face, and only visible after painting.
Two shifts went into gap and penetration changes. The pitch had already answered the question before anyone touched a dial.
Measure the Pitch Before Touching a Setting
A roll turns once per circumference of strip that passes it. Any defect on that roll therefore prints once every pi times the roll diameter.
Measure the distance between ten consecutive marks and divide by ten. On this job the marks sat 3,220 mm apart over ten intervals, so the pitch was 322 mm.
Divide the pitch by pi and the diameter appears: 322 divided by 3.1416 is 102.5 mm.
That is the diameter of the second upper work roll, which had been reground from 105 mm nominal six months earlier. The arithmetic took four minutes and the roll measurement confirmed it.
Measure along the strip with the line stopped, using a steel rule and a marker. Measuring between two marks only gives one interval, and one interval on a 322 mm pitch is easy to misread by 10 mm.
Ten intervals also average out the small variations caused by feed length error, which on a machine with 0.05 mm of slip per stroke accumulates to half a millimetre over ten pitches.
Write the pitch on the strip with a marker and keep the piece. It is the one piece of evidence that survives a shift change and settles the argument about which roll is at fault.
Photograph the mark with a rule alongside it. A 5 mm line on a 1,250 mm strip looks like a scratch in a photograph without a scale, and the depth estimate that follows is guesswork.
The Circumference Table That Names the Roll
Most straightener rolls fall into a narrow band of diameters, so a pitch measurement usually identifies one position in the stack.
| Mark pitch | Roll diameter | Where it usually sits | What it costs to ignore |
|---|---|---|---|
| 188 mm | 60 mm | Entry pinch roll or a small support roll | Edge marks on narrow strip, guide wear |
| 251 mm | 80 mm | Backup roll on a compact stack | Faint repeating lines that show after paint |
| 283 mm | 90 mm | Work roll on a light-gauge machine | 0.01 mm grooves, rejected at final inspection |
| 320 to 330 mm | 102 to 105 mm | Work roll on a 1,300 mm class machine | Strip scrapped at 5 to 8 percent of the run |
| 346 mm | 110 mm | Work roll on a heavier 5-roll stack | Marks deepen as the roll wears |
| 471 mm | 150 mm | Leveller roll or a large lower work roll | Long shallow marks, hard to see before paint |
| 628 mm | 200 mm | Feed roll or a large pinch roll | Slip marks combined with length error |
Two rolls can share a diameter, and then the pitch alone cannot separate them. That is where the tests in the next section take over.
On a 5-roll stack the three upper and two lower rolls often differ by a few millimetres, which is enough to tell them apart at 322 mm pitch.
Four Causes and the Test That Separates Them
Once the roll is named, four causes remain, and each one leaves a different signature on the strip.
Runout is the most common. A roll reground on centres but seated on a damaged bearing journal will orbit, and the mark depth varies with the high point.
Embedded debris is the second. A sliver of strip or a spot of weld spatter pressed into the roll face leaves a mark with sharp ends and a constant depth.
A flat spot is the third, and it comes from a coil break or a jam where the roll stopped against hot, hard material. The mark is wide and shallow rather than a line.
Pulsation is the fourth. A hydraulic or mechanical oscillation at roll frequency shows as a repeating wave rather than a discrete mark, and it usually disappears when the line runs empty.
- Dial indicator on the roll face, turned by hand: total runout under 0.01 mm passes
- Foil test: run 0.05 mm aluminium through and read the imprint against the roll
- Stop mid-strip and inspect the contact line, which shows whether the mark is continuous
- Open the top stack and run: if the mark disappears, the fault is in the upper rolls
- Swap two rolls of similar diameter and watch whether the pitch moves with them
The foil test is worth the twenty minutes it takes. Aluminium at 0.05 mm records a 0.005 mm defect that a dial indicator reads as noise and a painted panel shows as a line.
Marks That Follow the Coil, Not the Roll
Not every repeating mark comes from the machine. Some travel with the coil and repeat at a pitch far longer than any roll.
A coil break leaves a transverse band that appears once per coil revolution. On a 1,500 mm outside diameter coil that is 4,712 mm, which is ten times the roll pitch.
If the mark spacing changes when a new coil is loaded, the fault is in the material. If it stays at 322 mm across three coils, it is in the machine.
Slitter burr produces an edge condition rather than a line, and it repeats at the shear pitch of the slitting line, usually 300 to 600 mm but always at the edge.
Mill skin-pass marks and rust bands are the other two, and both are visible before the strip reaches the machine if anyone looks at the coil head.
Roll a metre of strip out on the floor before the line and inspect it. That single habit separates material faults from machine faults faster than any instrument.
What a Gap Change Cannot Fix
The instinct on any strip mark is to change the gap. On a roll defect that instinct makes the problem worse.
Reducing the gap increases the contact pressure on the defective roll, so the mark gets deeper and the scrapped length gets longer.
Increasing penetration does the same thing from the other direction. More work per pass means more pressure at the same defect.
Polishing the roll in place is the second trap. Hand polishing removes 0.01 to 0.02 mm from a high spot and takes the case depth with it, and the roll then wears into a hollow within a few months.
A shallow mark is also hard to prove. Below about 0.005 mm deep, a mark will not show on bare strip under workshop light and will appear only after painting, which is where the reject usually happens.
Finally, a stack with more rolls has more contact points. A 9-roll machine is not more likely to mark, but it has twice as many places for a mark to come from, and the pitch table gets longer.
The right repair depends on the cause. A roll with 0.03 mm of runout is reground, which costs 400 to 800 USD and takes the diameter down by 0.1 to 0.2 mm.
A roll with an embedded sliver is dressed by hand and returned to service in an hour, provided the high spot is under 0.01 mm afterwards.
A roll with a flat spot from a coil break is usually replaced, because grinding out a 0.05 mm flat removes enough material to change the pitch and the stack geometry.
Replace the whole set rather than one roll when the diameters have drifted apart by more than 0.5 mm. Mismatched diameters change the contact pattern and the flatness result.
It also means the next investigation starts from a worse position, because the pitch table no longer describes the stack.
Prevention at the Next Roll Change
- Record total runout on every roll at each change, not just when a mark appears
- Keep a spare set ground to the same diameter so a swap does not change the pitch table
- Fit a debris shield over the entry so slivers cannot reach the first work roll
- Store rolls on padded cradles, never on a concrete floor or against each other
- Check the felt or wiper contact strip at every shift, since it marks in a straight line
Roll count, pitch and gap interact, and the flatness side of that interaction belongs to our coil line knowledge base, not to a strip mark investigation.
FANTY has supplied straightening equipment to more than 60 countries, and the plants that keep strip clean tend to be the ones with a roll log.
The coil line equipment index lists model and roll configuration data for anyone checking a machine against a mark that has just appeared.
Is 0.02 mm of roll runout enough to mark 1.2 mm strip?
Yes. The target is 0.01 mm total indicator reading, because 0.02 mm is 1.7 percent of a 1.2 mm strip thickness and prints visibly.
Does a 0.005 mm mark show after painting?
That is roughly the threshold. Below it the paint covers the line, which is why marks are often found at final inspection rather than at the machine.
Does a 20-minute foil test confirm a roll mark?
It does, including the roll change. A 0.05 mm aluminium foil resolves defects down to about 0.005 mm on the surface.
Does a 9-roll stack mark strip more than a 5-roll stack?
Not more deeply, but it has four extra contact points, so the chance of one defective roll in the stack is higher.
Where to go next
A repeating mark is the easiest strip defect to diagnose, because the strip itself carries the measurement.
The flatness pillar treats roll count, pitch, gap and penetration as one system, which is the context a mark investigation needs before a roll is pulled.
Open the flatness specification guide