What Happens When a 3-in-1 Feeder Runs Thin Stock?
- Share
- publisher
- David Park - Senior Stamping Engineer, FANTY Machinery
- Issue Time
- Oct 12,2026
Summary
A plant bought a 6.0 mm line and ran 0.8 to 1.5 mm stock on it for most of the year, then faced flatness complaints on exactly those jobs. This field case follows the measurements, explains why large rolls cannot bend thin strip past yield, and lists the four setup changes that fixed it. It also states where a wide-range machine genuinely cannot help.
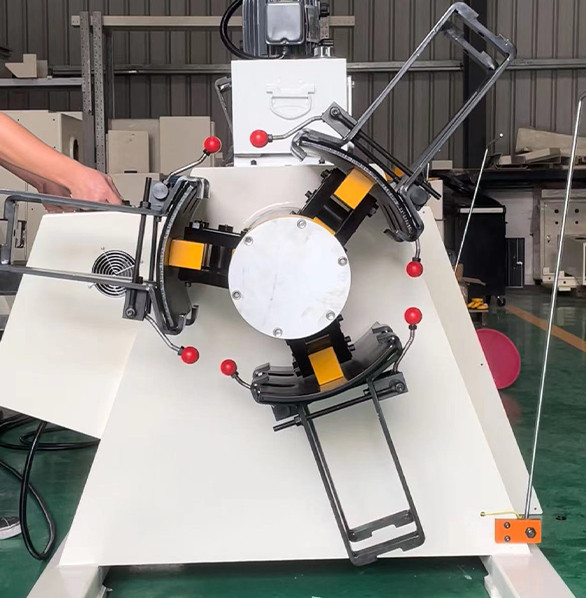
A stamper in Guangdong bought a line rated to 6.0 mm because the sales sheet said it could do everything.
Eighteen months later, 80 % of its running hours were on 0.8 to 1.5 mm stock, and the flatness complaints came from exactly those jobs.
Nothing was broken. The machine was doing what a wide-range machine does at the bottom of its range.
This is a field case about a 3-in-1 straightener feeder, what the measurements showed, and where a wide-range machine genuinely cannot help.
The Line and the Job It Was Hired For
The plant runs appliance brackets and electrical enclosures. Material is SPCC and SPHC, mostly 0.8 to 1.5 mm, with occasional 2.5 mm work for a different customer.
The line was specified at 1300 mm width and 6.0 mm maximum thickness, on the reasoning that headroom costs little and protects future orders.
Within six months the complaints were consistent. Parts from the thin-gauge dies failed a flatness check the customer ran with a straight edge and a feeler gauge.
Light marks also appeared on the visible face of the enclosure panels, on jobs that used prepainted stock.
The NC straightener feeder had not changed. The material mix had simply drifted towards the thin end of the range it was bought to cover.
None of the thick jobs had a problem. The line held them easily. Only the thin end of the range was failing.
What the First Measurements Showed
We measured four things before touching a setting, and three of them ruled out the obvious suspects.
Roll runout. Within 0.02 mm on every roll, which ruled out a damaged roll as the cause of the marking.
Roll surface roughness. Ra between 0.5 and 0.6 µm, consistent with a lightly used machine rather than a worn one.
Gap setting resolution. The finest repeatable adjustment was 0.05 mm, which is 6 % of the strip thickness on 0.8 mm stock.
Flatness after straightening. Between 3 and 5 mm of bow over a 1000 mm sample, measured with the die out of the line.
| Measurement | Reading | Expected for Thin Stock | What It Ruled Out |
|---|---|---|---|
| Roll runout | Within 0.02 mm | Within 0.02 mm | A damaged or bent roll |
| Roll surface Ra | 0.5–0.6 µm | 0.6–0.8 µm for thin coated stock | Excessive wear, but not polishing |
| Gap resolution | 0.05 mm steps | 0.02 mm or finer below 1 mm | Operator error as the main cause |
| Bow after straightening | 3–5 mm per 1000 mm | Under 1 mm | Die or feeder fault |
Two rows point in the same direction. The machine could not set a fine enough gap, and it could not apply enough work to a thin strip to remove the bow.
Why a Wide-Range Machine Struggles at the Bottom
Straightening works by bending the strip past its yield point, alternately, over a series of rolls. The amount of bend depends on roll diameter and roll spacing, not on how hard the machine can push.
Roll diameter is fixed. Rolls sized to survive 6 mm stock are large, and a large roll bends thin strip gently. The bend may never reach yield, so the bow survives.
Gap sensitivity rises. On 0.8 mm stock a 0.05 mm change is 6 % of thickness. On 6 mm it is under 1 %. The same screw resolution is coarse at one end and fine at the other.
Roll deflection matters less, marking matters more. Thin strip takes the roll's surface finish directly, so a roll that is fine for 3 mm leaves visible marks on 0.8 mm prepainted or coated sheet.
This is not a defect. It is what happens when one geometry has to serve a 7.5 to 1 thickness ratio.
The Four Changes That Fixed It
None of the fixes required a new machine, and together they took the flatness reading from 3–5 mm to under 1 mm per 1000 mm.
- Rewrote the setup sheet as two separate regimes, one for thin stock and one for heavy, instead of one compromise setting.
- Set the thin regime with less roll pressure and more penetration, so the work went into bending rather than into crushing the strip.
- Changed the lubricant to a lighter grade and reduced carry-over, which removed most of the visible marking.
- Added a flatness check at the line rather than at final inspection, so a bad setting is caught inside one coil.
The flatness method itself matters as much as the settings. Checking a 1000 mm sample under a straight edge at a shallow light angle finds bow that a feeler gauge on a 300 mm sample misses entirely.
The same procedure applied to the coil line product range is how we compare frames before a purchase.
The four changes are worth writing down as a regime, because the settings that suit 0.8 mm are wrong for 2.5 mm on the same machine.
| Setting | Thin-Stock Direction | What It Changes | Where It Costs You |
|---|---|---|---|
| Roll pressure | Lower | Less marking, more reliance on penetration | Too low and the strip slips between the rolls |
| Penetration | Higher | More bend per pass, so the bow is worked out | Excess penetration bows the strip the other way |
| Lubricant | Lighter | Less carry-over and less visible marking | Thin oil offers less protection against galling |
| Gap resolution | Finer steps | Settings can be dialled in rather than approximated | Finer adjustment is slower to set and easier to disturb |
Recording the regime as a table matters more than any single number in it. Two operators setting the same machine from memory land on different values, and the flatness result differs with them.
The cost column is the part most setup sheets omit.
Every thin-stock setting that improves flatness takes something back, usually grip or setup speed, and the operator making the trade should be able to see it written down.
Where a Wide-Range Machine Still Cannot Help
The fixes above worked because the thin end of the range was 0.8 mm, which is still a working thickness for this geometry. Push further and the honest answer changes.
Below roughly 0.5 mm, roll geometry wins. No combination of pressure and penetration will remove bow that the roll diameter never bent past yield. A narrower-range machine is the real answer.
Coated and prepainted stock has a harder limit. Even where flatness improves, the roll surface transfers its finish to the strip.
For visible panels, a roll set with a finer finish is a specification item, not a setting.
The two-regime approach costs setup time. Running thin and heavy work on the same line means two documented setups and a verification run at each changeover.
Plants that switch several times a shift sometimes find the changeover cost higher than they expected.
Marking can come from the coil, not the machine. Edge damage from handling and mill marks survive straightening, and no setting removes them, which is the diagnosis covered in roll settings that mark strip.
What We Changed in the Specification Next Time
The lesson was not that wide-range machines are wrong. It was that the range has to be matched to the material mix, not to the heaviest order anyone can imagine.
Weight the specification by running hours. If 80 % of hours are under 1.5 mm, the specification should be optimised for that band and treat 6 mm as the exception.
Ask for gap resolution as a number. A quotation that states the finest repeatable gap adjustment is easier to compare than one that says fine adjustment.
Specify the roll surface for the visible face. If the strip is prepainted or exposed on the finished part, roll finish belongs in the specification next to thickness.
Test at the bottom of the range. Acceptance tests run on the middle of the range prove nothing about the jobs that will actually pay for the machine.
FANTY has built more than 200 coil lines and the flatness discussion usually starts before the order, because a machine's useful range is narrower than its rated range.
The roll geometry behind that trade-off is set out in the coil line guide library.
At what thickness ratio, 4 to 1 or 8 to 1, does flatness start to go?
Beyond roughly a 4 to 1 ratio between the top and the working thickness, the bottom of the range needs its own settings. At 7.5 to 1, as in this case, it needs its own regime.
How fine should gap adjustment be for 0.8 mm strip?
0.02 mm or better. At 0.05 mm steps, each adjustment is 6 % of the strip thickness, which is too coarse to dial in a flatness setting.
Can roll pressure remove bow on thin strip?
No. Pressure increases contact but does not increase bend. Bow is removed by bending past yield, which depends on roll diameter and spacing.
How much flatness improvement can setup changes deliver, 1 mm or 5 mm?
In this case, from 3–5 mm of bow per 1000 mm down to under 1 mm, without changing any hardware. Below about 0.5 mm thickness, setup alone stops being enough.
Where to go next
Machine range is the first question in the flatness cluster. Roll count, pitch, gap and penetration come next, and they are laid out in the same guide.