Straightener vs Leveler: What Is the Difference on a Coil Line?
- Share
- publisher
- David Park, Senior Stamping Engineer at FANTY Machinery
- Issue Time
- Jul 29,2026
Summary
A straightener removes coil set and crossbow by bending the strip across its thickness. A leveler uses more, smaller, closely spaced rolls to also correct edge wave and centre buckle, which are length differences across the width. This guide separates the defect types, compares roll geometry and support, and lists what to ask for when specifying either machine.
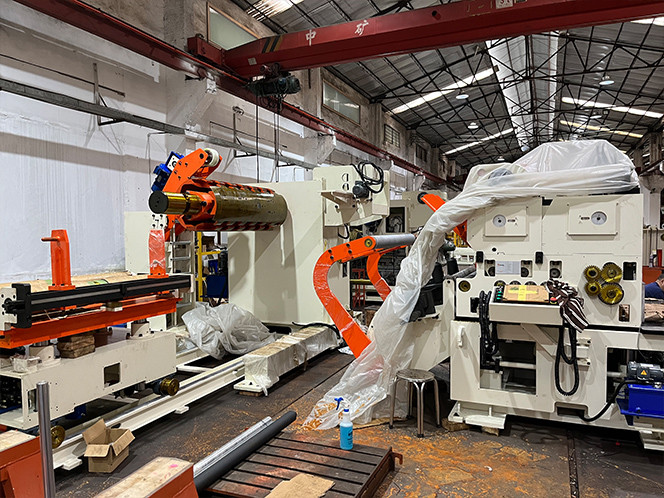
Ask two machine suppliers whether a coil line needs a straightener or a leveler and you will often get two confident, opposite answers. The confusion is understandable. The two machines look almost identical on the shop floor, both flatten metal that has been unwound from a coil, and neither term is standardised across the industry.
The distinction that actually matters is not the name on the nameplate. It is which defects the machine can remove, and therefore which defects will still be sitting in the strip by the time it reaches the die or the roll former.

Start With the Defect, Not the Machine Name
Coiled metal arrives at the straightener carrying several distinct shape problems, and they are not interchangeable. A machine that removes one of them perfectly can leave the next one completely untouched.
| Defect | What it looks like | Where it comes from | What actually corrects it |
|---|---|---|---|
| Coil set | Lengthwise curvature that stays in the strip after the coil is unwound | Residual stress locked in by winding at the mill | A straightener, when it is sized correctly for the thickness and yield strength |
| Crossbow | A curve across the width, so the strip forms a shallow smile or frown | A stress difference between the top and bottom surfaces | A straightener with enough roll support; stubborn cases need a machine with more corrective range |
| Edge wave | Wavy edges, because the edges of the strip are effectively longer than the centre | Uneven length across the width, often introduced at slitting or by tension | A leveler. A conventional straightener has no way to add or remove length |
| Centre buckle | A raised or wavy zone running down the middle of the strip | The centre of the strip is longer than its edges | A leveler with work-roll support and, in many cases, zoned adjustment |
| Camber | The strip curves sideways in its own plane rather than up or down | Usually created upstream, in slitting or in the coil itself | Often not correctable by a roll machine at all. Check the upstream cause before buying anything |
| Twist and mixed shape | Several errors combined along the length and across the width | Accumulated stress plus handling damage | Needs a defect map and a trial. One roll setting rarely removes every component at once |
Read that table down the fourth column and the whole debate collapses into one line. Coil set and crossbow are longitudinal, through-thickness problems, and a straightener is built for exactly those. Edge wave and centre buckle are length problems across the width, and no amount of roll penetration will ever fix a length difference.
One warning before going further. These words are not used consistently across the industry. Machines sold as precision levelers turn up inside press feed lines, and some heavy straighteners carry roll support that would embarrass a leveler. Compare the roll drawing and the capacity data for the exact model in front of you, not the label on the cover.
The Mechanical Difference Between the Two Machines
Both machines work on the same physical principle. As the strip passes through the work rolls it is bent up and then down, and if the outer fibres are pushed past yield, the stress pattern left in the material is more even than the one that went in.
| Feature | A press-feed straightener | A precision leveler | What the difference costs you |
|---|---|---|---|
| Work roll count | Typically 3 to 7 rolls | Typically 7 to 21 rolls | More rolls redistribute stress far better, but add purchase cost, setup time and more bearings to maintain |
| Roll diameter | Larger, sized to the heaviest strip | Smaller and closely spaced | Small rolls bend the strip more sharply per pass. They also deflect more, which is exactly why support becomes the limiting factor |
| Roll support | Simpler backing, sized to the frame | Substantial backup rolls along the work rolls | Backup rolls are what keep a small roll's geometry honest across the full width. Without them a long roll simply bows away from the strip |
| Adjustment | Entry and exit depth, roll gap and penetration | Adds multi-zone or segmented adjustment across the width | Zoned adjustment is powerful, but it needs an operator who understands what each zone does to the strip |
| Line position | Between the uncoiler and the feeder | Stand-alone, or inside a coil, blanking or cut-to-length line | Line position follows from whether the strip has to stay continuous or can be cut first |
| Acceptance focus | Stable die entry and reliable feeding | A defined flatness and residual-stress result | Whichever machine you buy, write the measurable target before you write the order |

Why Closely Spaced Rolls Change What Is Possible
Think about what happens inside the machine rather than what it is called. When the strip is bent around a small roll, the outer surface has to travel a longer path than the neutral axis. Bend it the other way on the next roll and the same thing happens in reverse.
A leveler exploits exactly this. By using many closely spaced rolls of small diameter, it can force specific bands across the width to stretch slightly more than their neighbours. Those bands then match the length of the rest of the strip, and a length problem such as edge wave or centre buckle starts to disappear.
A straightener cannot do that, and it is not a design flaw. With fewer, larger rolls, the bend is distributed broadly across the face of the strip instead of being concentrated in narrow zones. That is precisely the right behaviour for removing crossbow and coil set, because those defects are uniform across the width.
It is the wrong behaviour for correcting a length difference that varies from edge to centre.
| Question to ask | If the answer is yes | If the answer is no | The consequence |
|---|---|---|---|
| Is the defect mostly lengthwise curvature? | A straightener is the efficient answer | Look at a leveler before you look at roll penetration | Buying a leveler for pure coil set spends money on capability the strip never uses |
| Is the flatness measured as a length difference across the width? | A leveler is the only machine that can influence it | A straightener is sufficient | Chasing edge wave with a straightener usually ends in over-penetration and surface marking |
| Can the machine be run with backup roll support? | Small rolls can hold geometry across a wide strip | Wide, thin strip will deflect the rolls and read as uneven across the width | Support, not roll count, is often what limits a wide line |
| Does the downstream process tolerate residual stress? | A straightener result is usually acceptable | Leveling or stress relief should be part of the specification | Residual stress shows up later as distortion after forming or in service |
What Each Machine Can and Cannot Fix
The table below is the shortest honest summary of the two technologies. The last column matters as much as the first three, because every gain in corrective capability is paid for somewhere.
| Defect | A straightener | A leveler | What you give up |
|---|---|---|---|
| Coil set | Removes it when correctly sized | Also removes it | Nothing. Both machines handle this well |
| Crossbow | Handles moderate cases | Handles it more thoroughly, especially on wide strip | The leveler costs more and needs the width to justify it |
| Edge wave | Cannot correct it | Corrects it by redistributing length across the width | Levelers are slower to set up and far less forgiving of a wrong setting |
| Centre buckle | Cannot correct it | Corrects it, particularly with zoned adjustment | Zoned control adds operator skill to the maintenance burden |
| Camber | Not a roll-correction problem | Usually not correctable either | Money spent here is often wasted; the cause is upstream |
| Residual stress pattern | Improves it near the surface | Redistributes it through the thickness | The leveler's advantage only pays if the downstream process actually needs it |
| Surface finish | Fewer roll contacts, lower marking risk | More roll contacts, higher marking risk on coated strip | Coated or pre-painted stock may need roll finishes chosen specifically for it |
Notice the pattern in the last column. Every additional capability a leveler brings is bought with money, setup time, operator skill or surface risk. That is why the correct question is never which machine is better in the abstract, but which defects your material actually carries and which of them your downstream process can tolerate.
When a Straightener Is Enough on a Press Feed Line
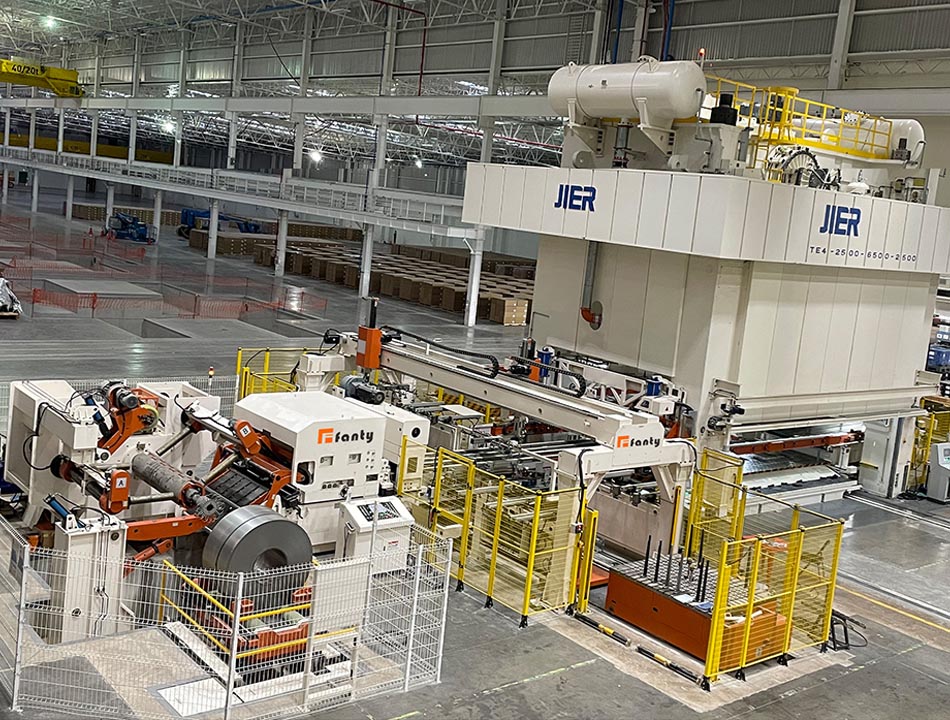
On a stamping line the straightener's job is narrower and more specific than a leveler's. It has to deliver strip to the feeder that is flat enough and stress-balanced enough to index repeatably into the die, coil after coil. That is a different requirement from producing a certified flatness result on a cut sheet.
In practice a straightener is the right machine when the incoming defects are dominated by coil set and crossbow, when the strip is fed continuously into a press, and when the acceptance criterion is stable die entry rather than a measurable flatness figure.
It is also the right machine when changeovers are frequent, because a 5-roll head can be set and verified faster than a 17-roll leveler.
Two conditions should make you stop and reconsider. The first is a strip that reads wavy at the edges or buckled down the middle no matter how the rolls are set. The second is a downstream process that reveals distortion after forming, which points at residual stress rather than at incoming shape.
Both conditions are leveler territory, and pursuing them with a higher roll count straightener will not solve them.
When a Straightener Reaches Its Limit
There is a moment on every press feed line where more roll penetration stops helping. Recognising it early saves strip, tooling and a great deal of arguing, because the symptoms are specific and they point in one direction.
| Symptom | What it usually means | The honest next step |
|---|---|---|
| Edge wave stays after the gap and penetration are reset | The defect is a length difference, which a straightener cannot influence | Specify a leveling stage rather than another roll on the straightener |
| Flatness improves then reverses as penetration is added | The strip is being over-bent and taking a reverse set | Back the penetration off and set the entry and exit depths as a pair |
| Roll load keeps climbing while the reading stops improving | The machine is at the edge of its capacity for that grade | If more than roughly 80 per cent of the available penetration travel is in use, the frame is the limit, not the setting |
| Scratches or marking appear on coated strip | Roll contact pressure or roll finish, not flatness | Check work roll material and finish before adding more correction |
| Distortion shows up only after forming or after a few days | Residual stress is being released downstream | This is a stress-distribution problem. Roller leveling is the technology designed for it |
The expensive mistake is treating a leveler problem with straightener settings. Each additional pass at higher penetration puts more load through the rolls, more marking risk onto the surface and more work hardening into the strip, while the defect that prompted the change survives untouched.
What to Ask For When You Specify Either Machine
When two quotations arrive, they are usually compared on width, thickness and price. Those three numbers say almost nothing about whether either machine can meet the flatness target. Ask for the following instead, and compare the answers rather than the covers.
- Work roll diameter and the pitch between rolls, for the exact model. These two numbers decide how sharply the strip is bent and how many times. Roll pitch is covered in detail in this guide to choosing roll pitch.
- Number of work rolls, and whether the layout is symmetric.
Roll count is not a quality score on its own; it has to match the thickness and the defect you are chasing. - The backup and support arrangement, and how roll deflection is limited at the full rated width.
This is where wide, thin strip is usually lost. - The adjustment method, in numbers: how much travel is available at the entry and exit rolls, and whether adjustment is across the full width or zoned.
- The drive rating and the capacity curve against yield strength, not a single maximum thickness figure quoted for mild steel only.
- The material, sample and measurement method behind any claimed flatness result.
A flatness figure without a datum and a verification method is a marketing number. - The maximum and minimum thickness the line will actually run, not the average.
Selection is driven by the extremes. - Coil inside diameter and the severity of the incoming coil set, because a tight-wound coil asks far more of the first pass through the machine.
If the machine is feeding a press continuously, the drive and control choice matters as much as the roll geometry.
Frequently Asked Questions
Is a leveler always better than a straightener?
No. A leveler can correct a wider set of defects, but that extra capability is paid for in purchase cost, setup time, operator skill and surface contact. If your incoming defects are coil set and crossbow and your acceptance criterion is stable die entry, a correctly sized straightener does the job with less to maintain.
Can a straightener remove edge wave or centre buckle?
Not reliably. Both are length differences across the width rather than curvature through the thickness. A roll straightener redistributes stress but has no mechanism to make one band of the strip longer than its neighbour, which is what correcting a length difference requires.
How many rolls should each machine have?
A press feed straightener typically uses 3 to 7 work rolls. A precision leveler typically uses 7 to 21, with smaller diameter rolls set closer together. Above roughly 2.5 to 3 mm in higher-strength grades, roll count and frame stiffness have to rise together, because the force needed grows faster than the roll geometry alone can handle.
Do I need a leveler for pre-painted or coated strip?
Usually the opposite. Every extra roll contact is another chance to mark the surface, so a high-roll-count leveler increases the risk unless the roll finish and contact pressure are chosen specifically for coated stock. Coil set on coated strip is often better handled by a straightener with the right roll surface.
What flatness can I expect from either machine?
That depends on the strip, the defect mix and how flatness is measured. There is no universal figure that applies across thicknesses and grades. Any claimed result should come with the material it was achieved on, the sample method and the measurement datum. Our guide to the flatness a straightener can achieve covers how to set that up properly.
I am not sure which defect I have. Where do I start?
Describe the shape rather than the machine. Is the curve along the length, across the width, or at the edges only? Does it change when the strip is measured free of tension? Those three answers narrow the choice faster than any specification comparison.
Where to go next
Once the defect is identified, most of the remaining work is roll geometry and setup rather than machine type. The cluster overview collects the guides that cover those settings in order.
Read the 3-in-1 decoiler straightener feeder guide